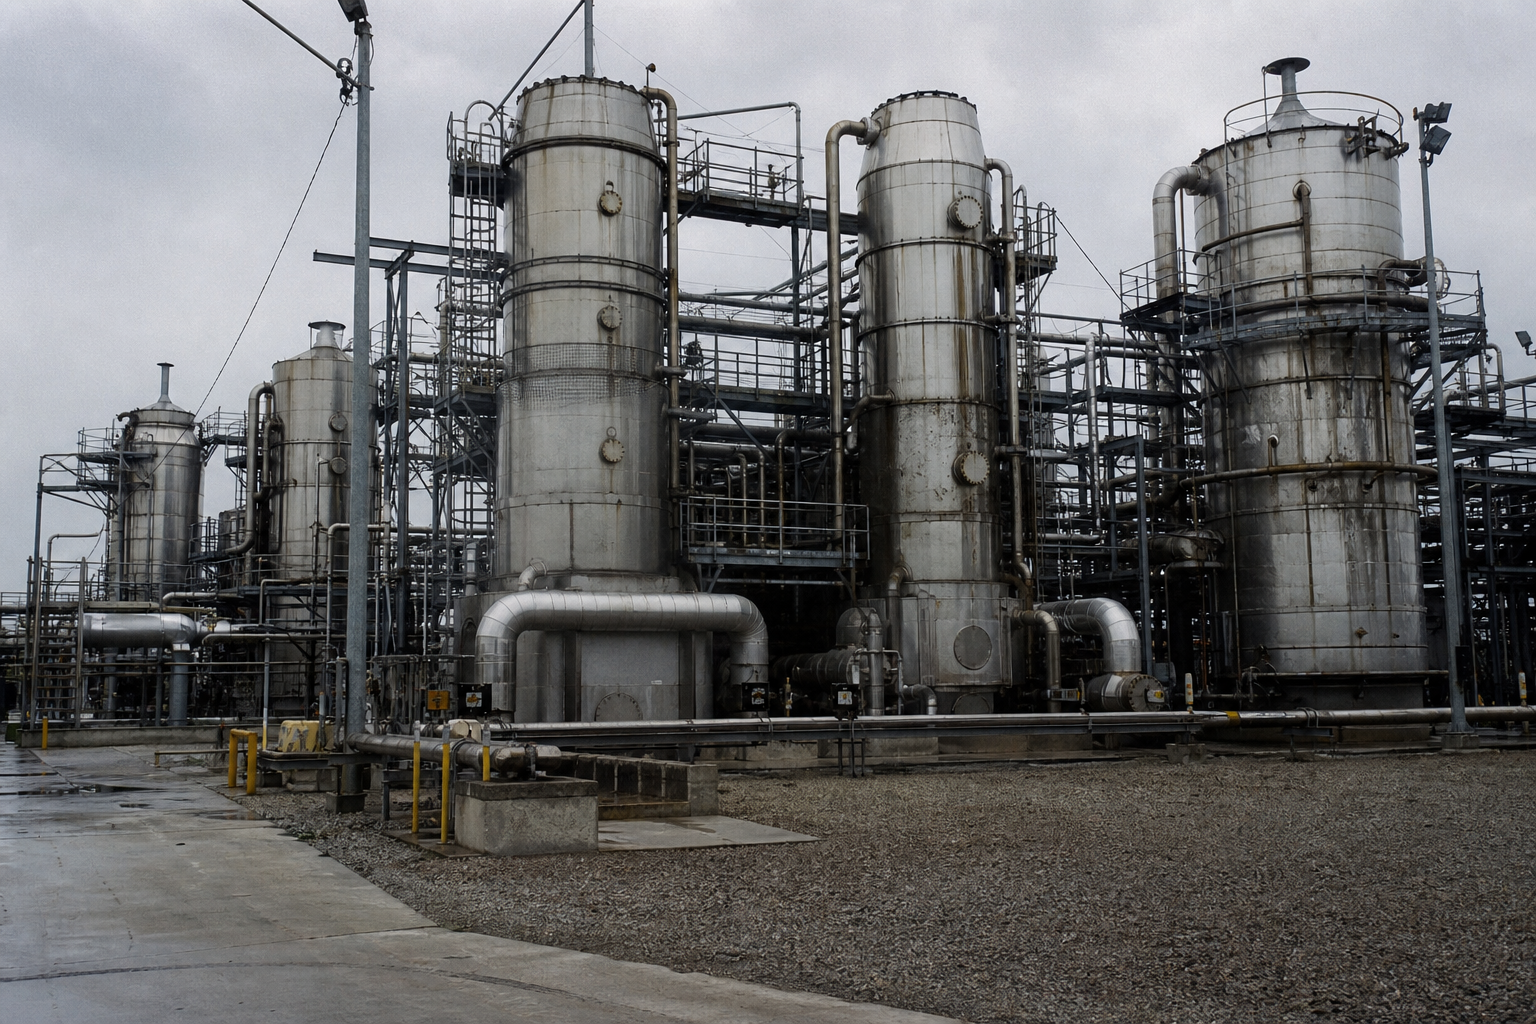
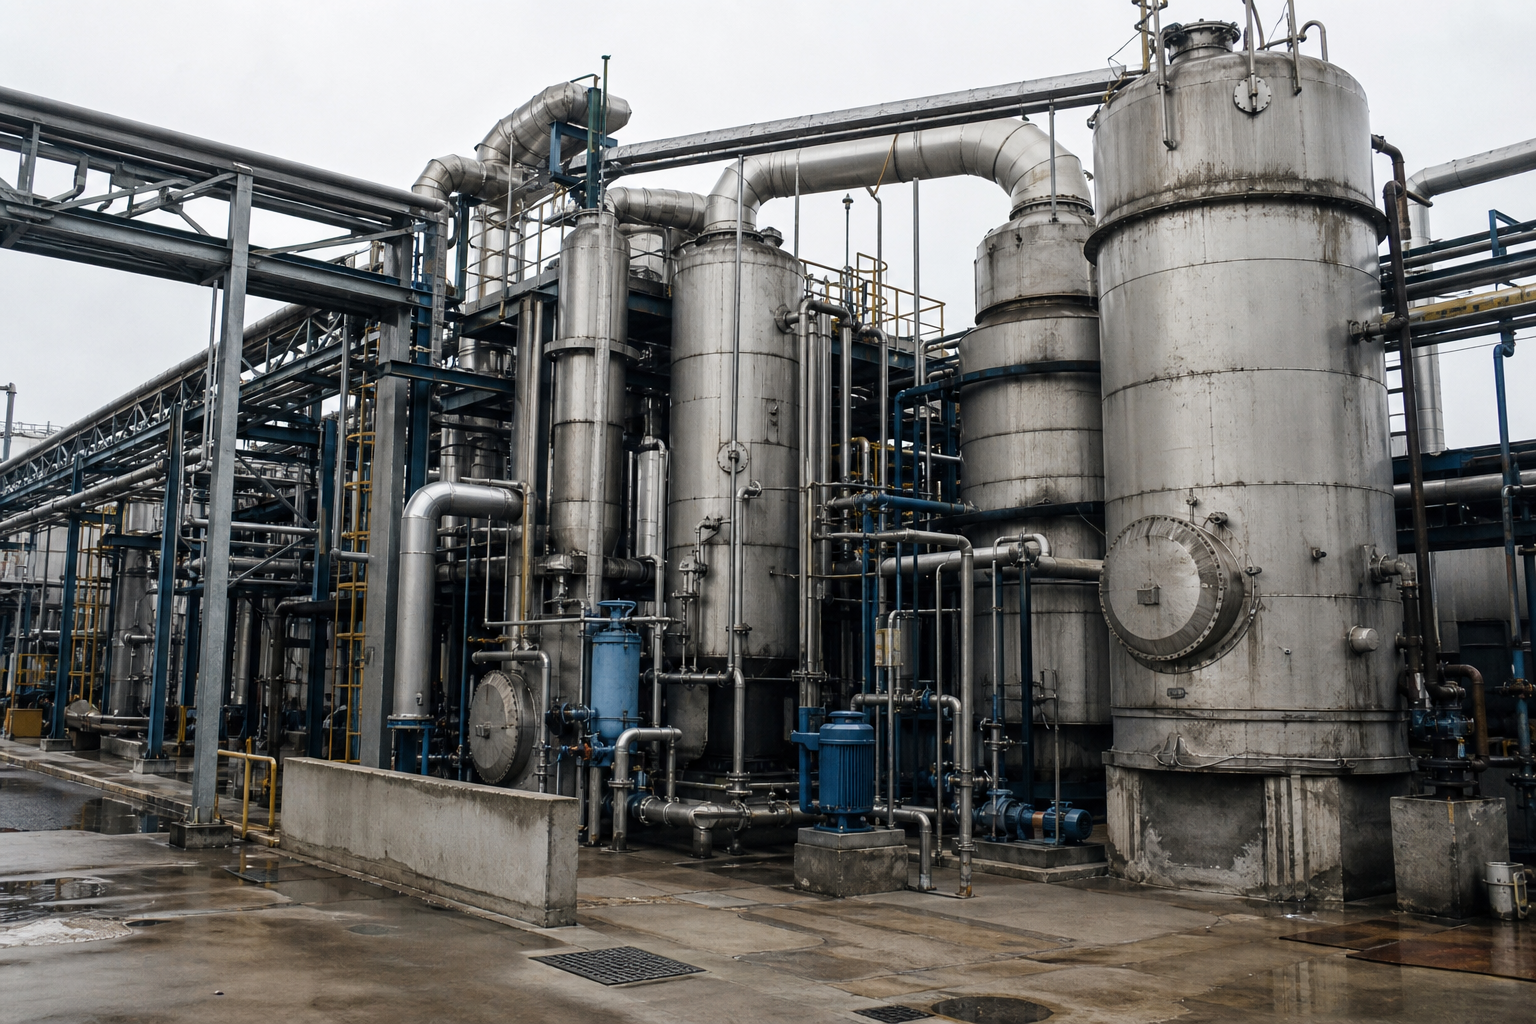
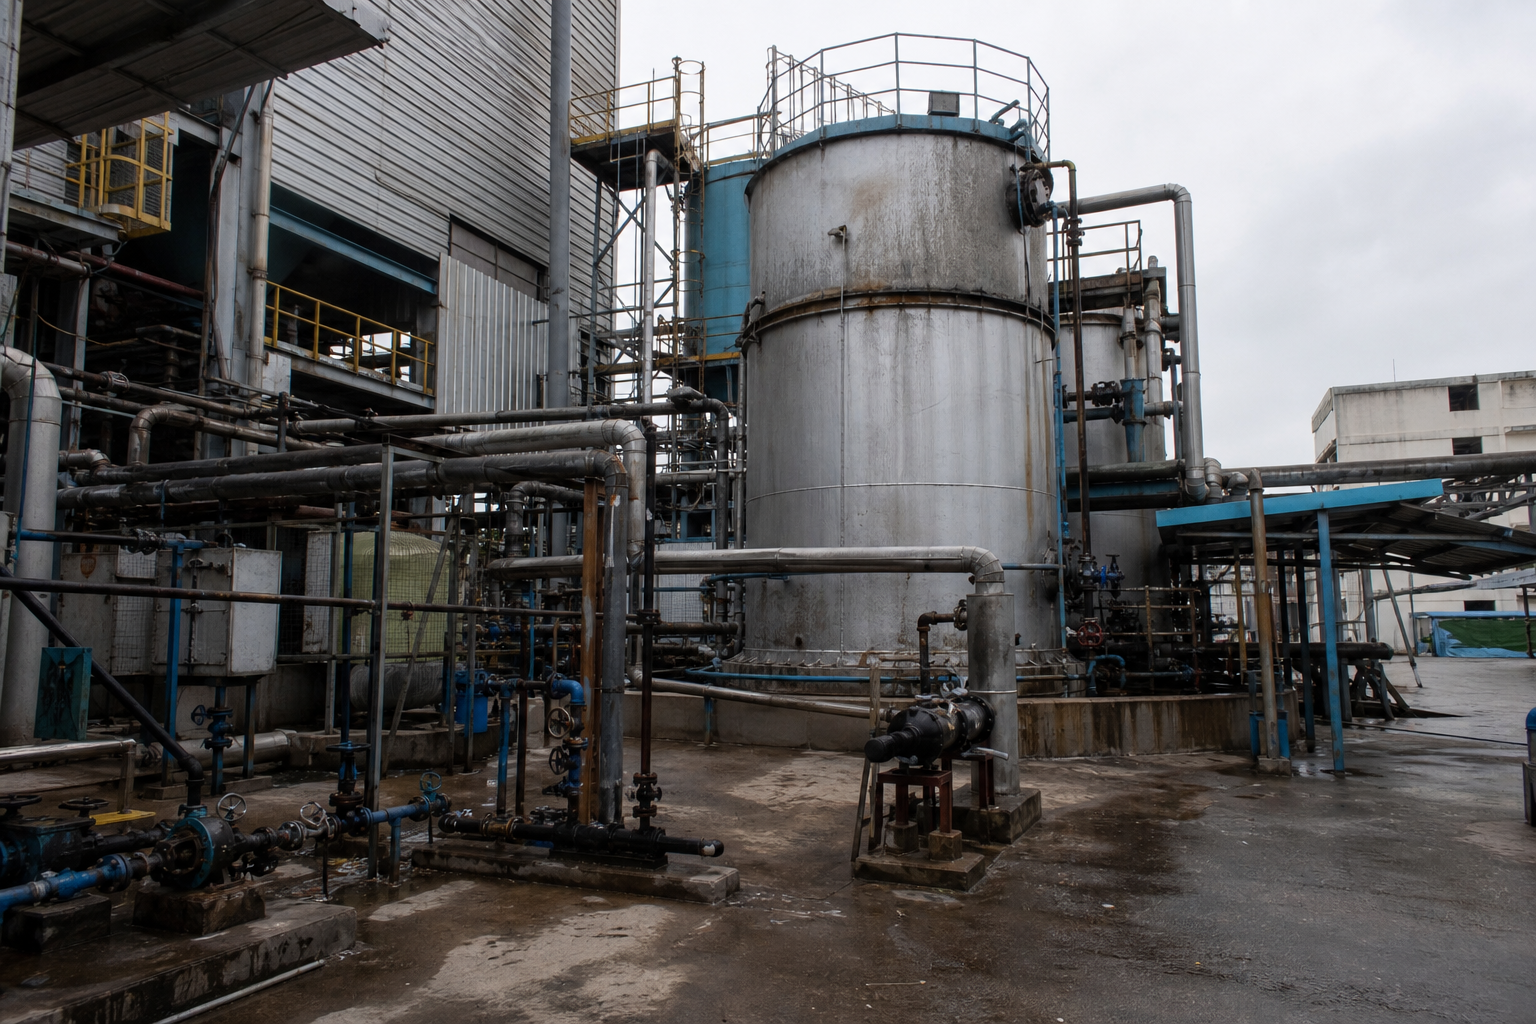
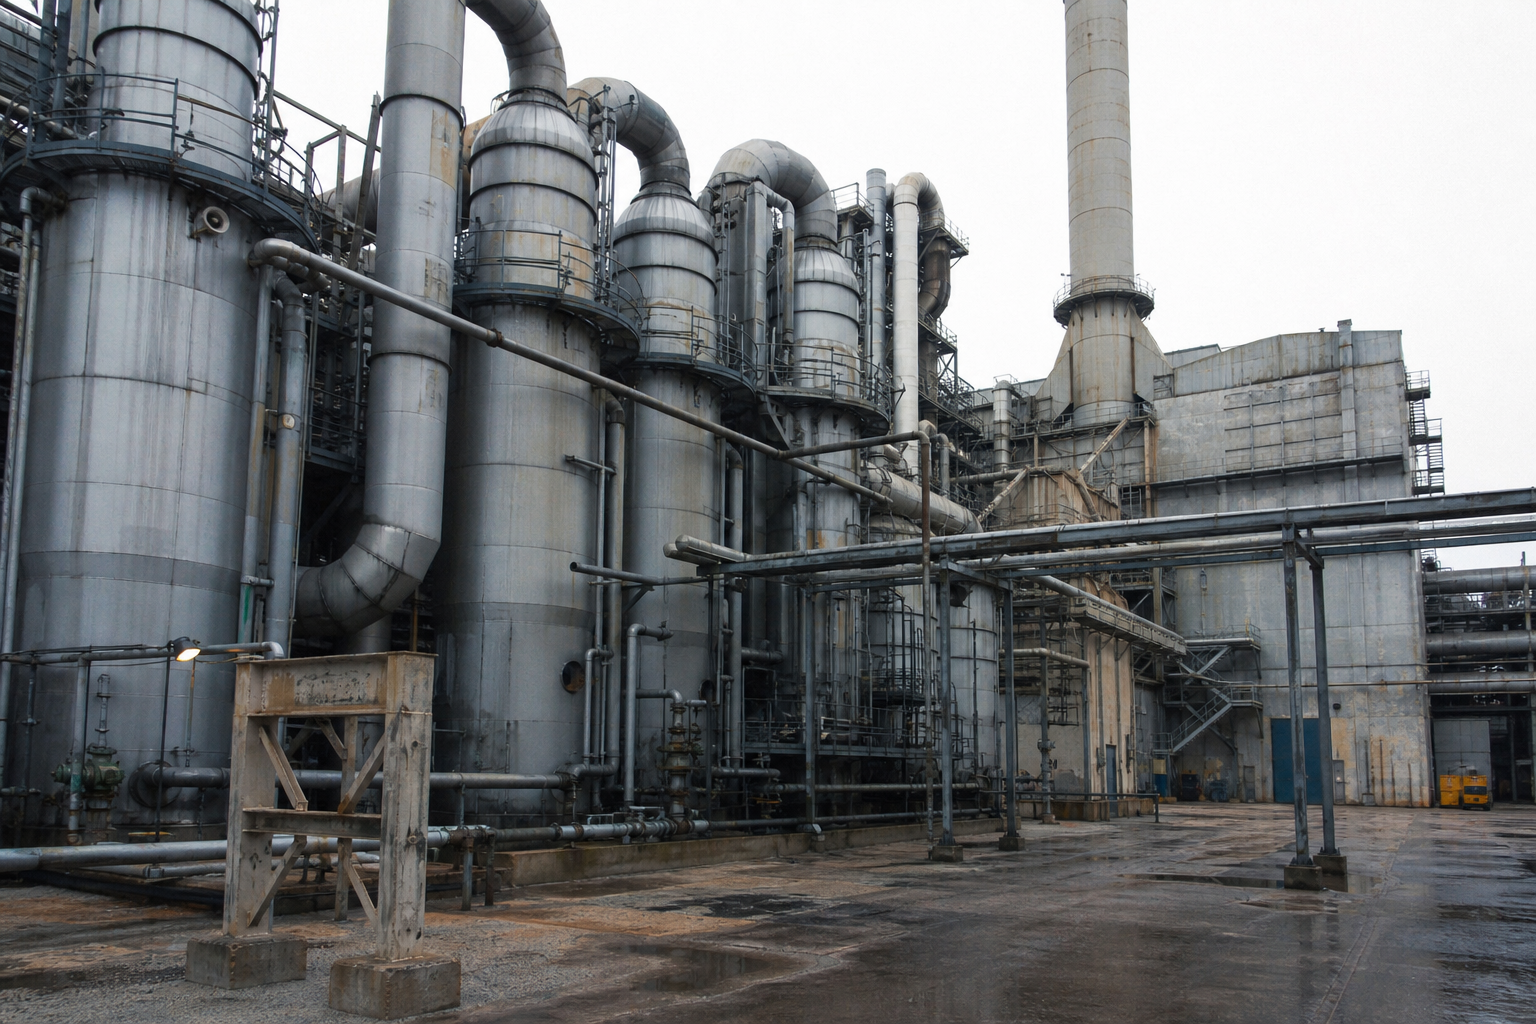
Industrial Evaporation, Concentration & Crystallization Systems
For wastewater minimization, process concentration, resource recovery and energy-efficient upgrades.
We engineer complete systems around your feed characterization, product specification and site utilities — from high-TDS brine minimization and product crystallization to MVR retrofit on existing evaporator trains.
From compliance-driven ZLD on mixed-salt brines to product-grade crystallization with controlled particle size — four scenarios where we hold proven operating references.
ZLD PROCESS TRAINPFD · SALT SPLITTING
SOLUTION 01Compliance-Driven
High-Salinity Wastewater Minimization & ZLD
Compliance, volume reduction and salt-by-salt recovery for high-TDS wastewater streams from coal chemical, battery, pesticide and chlor-alkali plants — including mixed NaCl / Na₂SO₄ systems and RO concentrate.
Process Liquid Concentration & Product Crystallization
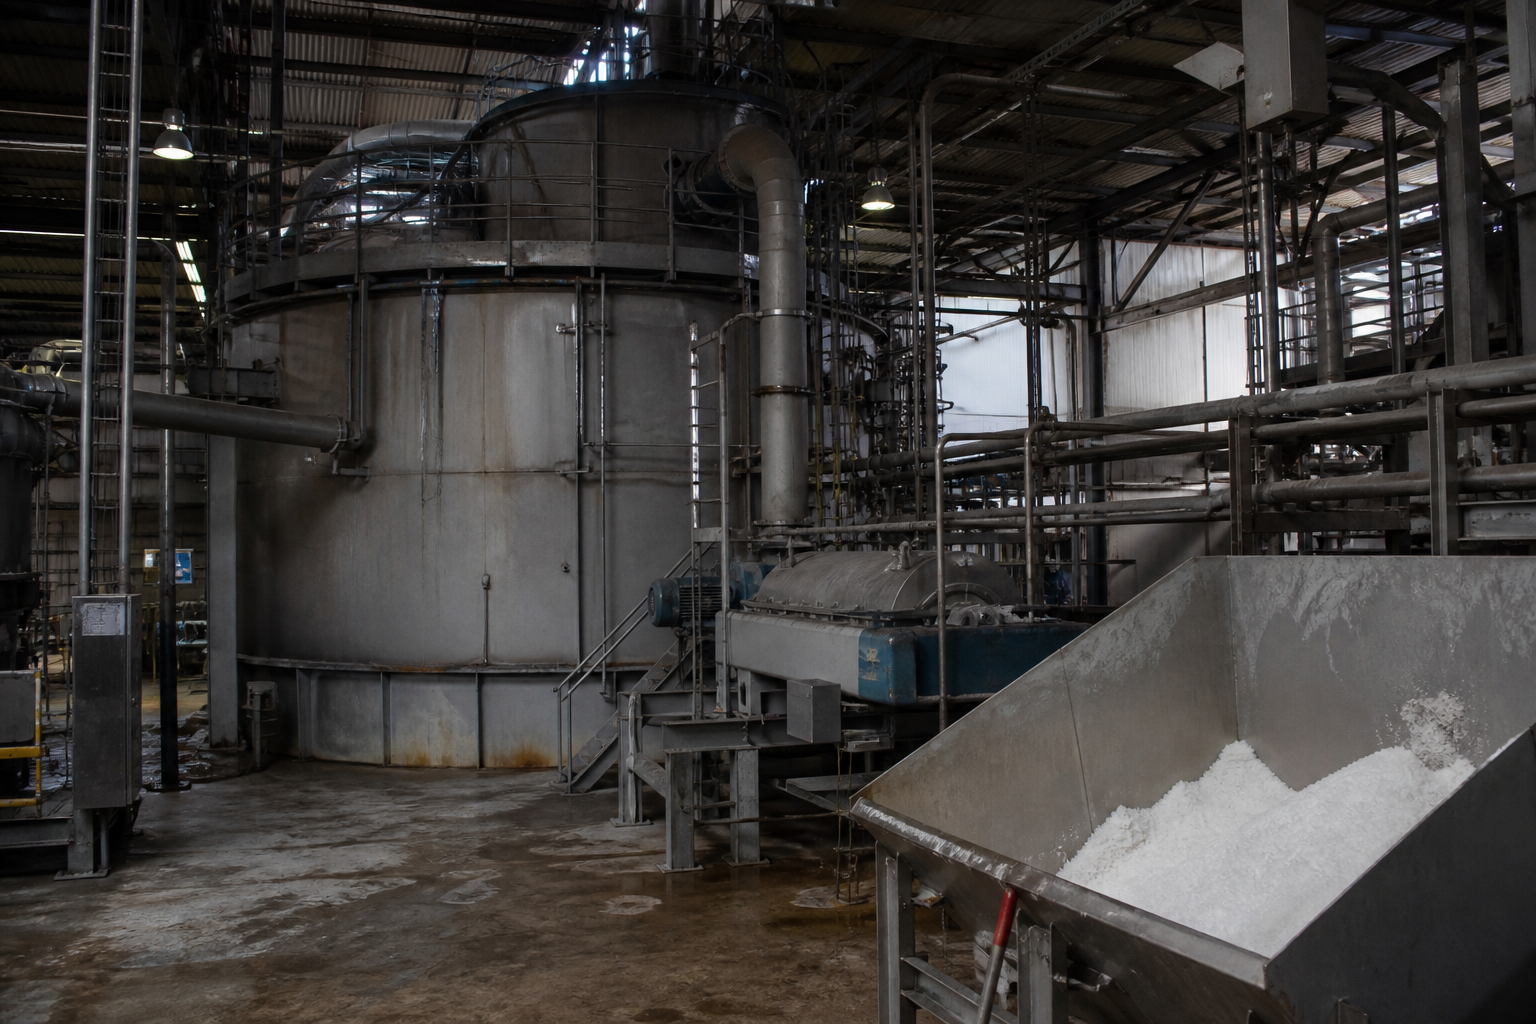
Concentration and product-grade crystal generation from process liquors, fermentation broths and hydrometallurgical solutions — including battery-grade Li₂CO₃ / LiOH, fertilizer-grade (NH₄)₂SO₄, organic acids and amino acids.
Recover dissolved product from mother liquors through controlled recycle, secondary crystallization and purge optimization — while managing impurity accumulation and protecting product PSD, purity and yield.
Recycle vs purge vs secondary crystallization decisions
Impurity accumulation modeling and purge stream design
Yield vs purity trade-off, quantified per chemical system
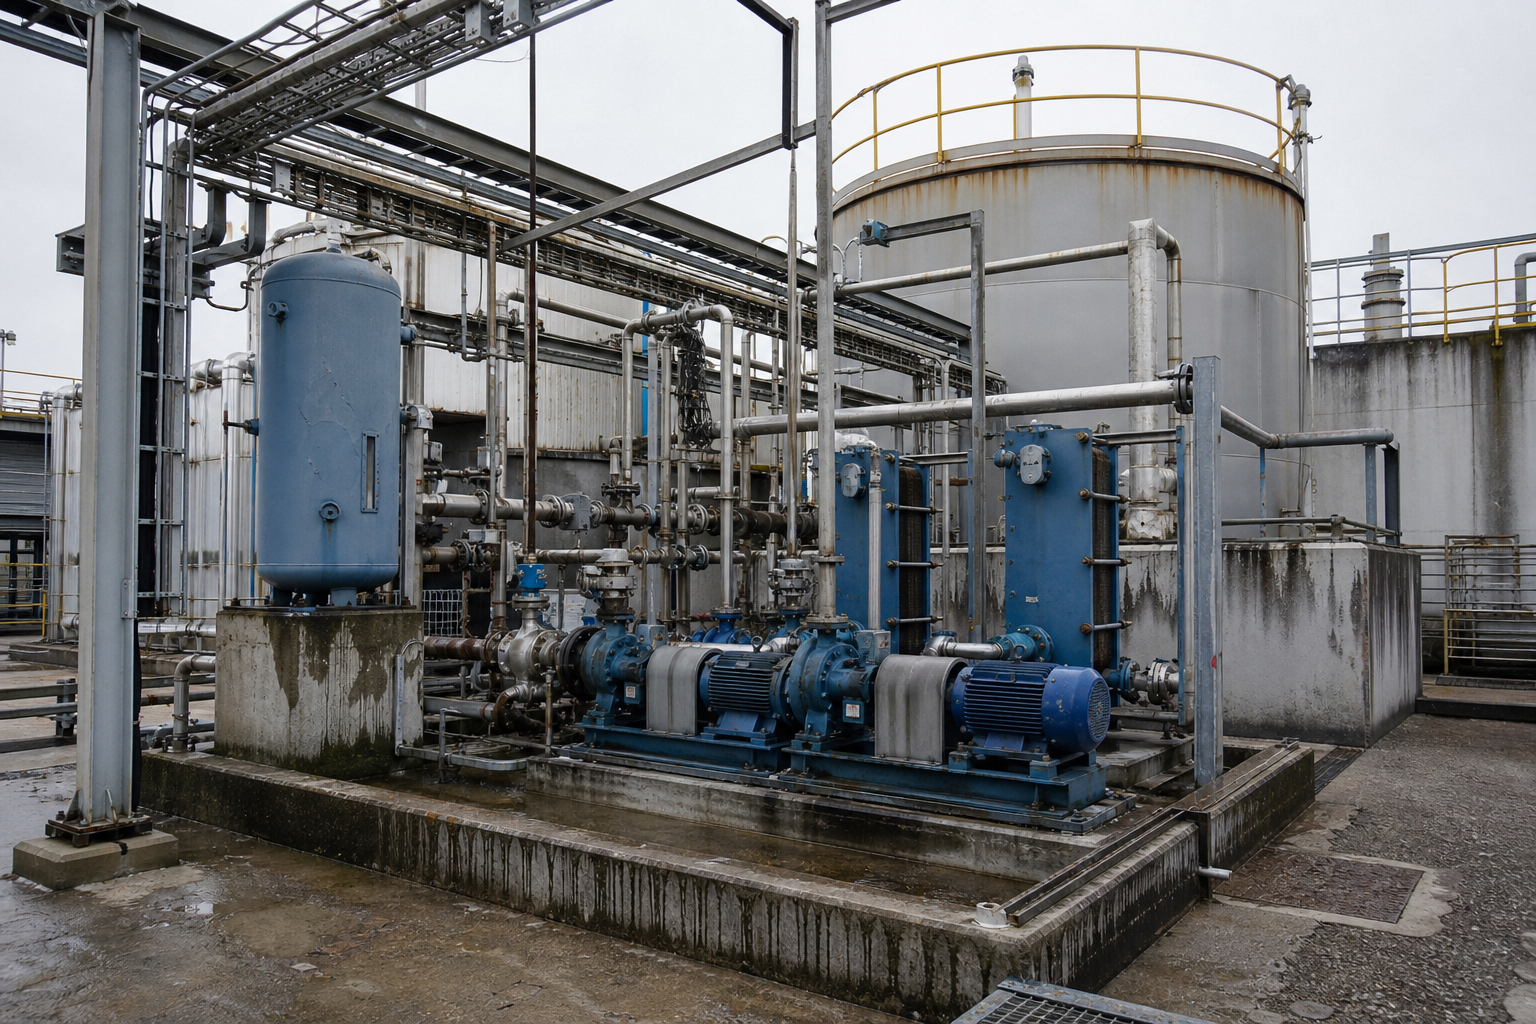
Reduce steam demand, debottleneck capacity and decarbonize existing evaporator trains approaching their economic limit — through MVR integration, TVR upgrade, heat recovery or adding an effect, without full system replacement.
MVR / TVR retrofit vs new multi-effect evaluation
Heat integration, condensate recovery and steam-header limits
Scope 1 reduction path under EU ETS / CBAM exposure
Battery-grade lithium salts (Li₂CO₃, LiOH·H₂O) to Ni / Co / Mn sulfate crystallization and LIB black-mass hydrometallurgy — engineered for >99.5% purity.
Pharmaceuticals & fine chemicals are served case-by-case under GMP-grade requirements — every vertical above has a dedicated hub.
Capabilities
Engineering from Process Design to Lifetime Support
A single accountable partner across testing, fabrication, commissioning and remote support — with English-language documentation for international clients.
01
Testing & Validation
Feed characterization (TDS, COD, viscosity, pH), solubility mapping, impurity profiling, corrosion coupon testing and bench-scale crystallization trials — before equipment is specified.
02
Quality & Fabrication
Heat and mass balance, PFD / P&ID development, equipment sizing and 3D layout — executed into material-traceable, code-compliant fabrication.
03
Delivery, FAT & SAT
Pressure testing, factory acceptance test, shipment, site installation and commissioning — performance verified against guarantee curves at sign-off.
04
Remote Support
Remote diagnostics, lifetime spares, English-language O&M documentation and process support — with committed response times for international clients.
Four principles behind every system we engineer — and operating references on the difficult streams other suppliers decline to quote.
01
Process-First Engineering
Every project starts from feed characterization (TDS, COD, viscosity, impurity profile), product targets and site utilities. Energy strategy, evaporator configuration and crystallizer type follow the process — not the other way around.
We evaluate energy reuse (MVR / multi-effect / TVR), process configuration (falling film / forced-circulation), supersaturation method and crystal growth configuration (FC / DTB / Oslo) as four orthogonal decisions — not a single catalog lookup.
A single accountable partner across feed assessment, bench-scale feasibility, PFD development, FAT, SAT commissioning and lifetime support — with documentation and remote diagnostics built for international projects.
All tools give indicative first-pass results only — final design requires feed characterization and project-specific engineering evaluation.
Ready to Discuss Your Project?
Send us your feed characterization (TDS, COD, main salts, viscosity), throughput and product targets — we will respond with a preliminary process route and indicative sizing within two business days.
Send your feed characterization (TDS, COD, main salts, viscosity), throughput and product targets — we respond with a preliminary process route within two business days.