
EvapCryst logo

DTB — Draft Tube Baffle Crystallizer

Product quality first. An internal draft tube directs circulation while a baffle separates the growth zone from a fines-removal zone — classified-fines destruction produces large crystals (0.5–2 mm) with a narrow distribution that centrifuges easily and carries little mother liquor.

Draft tube baffle DTB crystallizer for controlled crystal growth
At a Glance

Four Numbers That Define DTB

Reference ranges under typical operating conditions on inorganic salt systems.

Crystal Size (d50)
0.5–2.0 mm
larger crystals with controlled distribution — classified-fines removal keeps the PSD narrow
Draft Tube Velocity
1–2 m/s
internal circulation velocity through the draft tube — controllable, and it sets the growth-zone environment
Baffle Gap Velocity
0.5–1 m/s
velocity in the baffle annulus — the fines-removal (elutriation) zone that separates fines from product crystals
Slurry Density
15–30 wt%
controllable slurry-density band — a primary lever on crystal size and PSD
Working Principle

Grow Inside the Draft Tube, Remove Fines at the Baffle

Two zones, two jobs: the draft tube circulates the growing crystal population; the baffle annuity classifies it — fines leave, product stays.

Simplified DTB Flow Diagram

Slurry → Draft tube (1–2 m/s growth circulation) → Baffle annulus (0.5–1 m/s fines elutriation) → Fines dissolved/removed → Product crystals to discharge

Fines removed at the baffle are dissolved and recycled — the crystal population that remains grows into the narrow, large-crystal distribution DTB is known for.

01

Draft Tube Circulation

The internal draft tube directs flow at a controlled 1–2 m/s — the growing population stays suspended and mixed.

02

Growth Zone

Inside the draft tube, crystals grow under controlled supersaturation delivered by the Dimension C method of the plant.

03

Fines Removal Zone

The baffle annulus runs at 0.5–1 m/s: fine crystals are elutriated out, dissolved and returned — keeping them out of the product.

04

Classified Discharge

Product crystals leave at 0.5–2 mm — narrow PSD, easy centrifugation, little mother-liquor carryover.

Configuration Selection

FC vs. DTB vs. Oslo

Three vessel configurations, three priorities: FC puts engineering reliability first, DTB puts product quality first, Oslo puts crystal quality first.

ParameterFCDTB (this page)Oslo
Selection priorityEngineering reliabilityProduct quality (narrow PSD)Crystal quality (large, pure)
Typical crystal size0.2–0.8 mm — moderate, wide distribution0.5–2.0 mm — larger, controlled1.0–5.0 mm — large, very uniform
Fines removalNone standard — no internal classificationYes — classified-fines removal loop (elutriation zone)Natural — classification by fluidization
Circulation velocity2–3 m/s external loop1–2 m/s internal draft tube0.02–0.05 m/s fluidization upward velocity
Supersaturation toleranceHigh — recirculation dilutesMedium — controlled by draft-tube velocityLow — ≤1–2 g/L to avoid spontaneous nucleation
Best forHigh-salinity, scaling-prone, mixed-salt systems: NaCl, Na₂SO₄, ZLD mixed saltsFertilizer (NH₄)₂SO₄, KCl, battery-grade Li₂CO₃ precursor, organic acidsBattery-grade NiSO₄ / CoSO₄ / MnSO₄, pharma intermediates, electronic-grade salts

d50 ranges reflect typical operating distributions on inorganic salt systems; actual PSD depends on residence time, fines management, seed control and the cooling/evaporation profile.

Chemical Systems

Where DTB Is the Standard Configuration

Chemical systems where large crystals with narrow PSD justify classified growth.

ChemicalRecommended configurationWhy
Ammonium sulfate (fertilizer grade)DTB / OsloFertilizer-grade spec demands large granules — the reference DTB duty
UreaDTBFertilizer-grade large-granule standard process
Potassium chlorideDTBPotash-industry standard
PTADTB / cooling crystallizationLarge-capacity continuous crystallization
Oxalic acidDTB / continuousContinuous crystallization replacing batch operation
Battery-grade Li₂CO₃DTB (growth stage)Reaction precipitation followed by DTB growth in the reference route

Chemical-configuration mapping from the crystallizer-type technical reference; final selection requires solubility data, impurity profiling and crystallization trials.

Selection

When to Pick DTB — and When Not To

DTB is the answer when product spec (PSD, centrifuge yield, mother-liquor carryover) is the priority and the feed is not extreme.

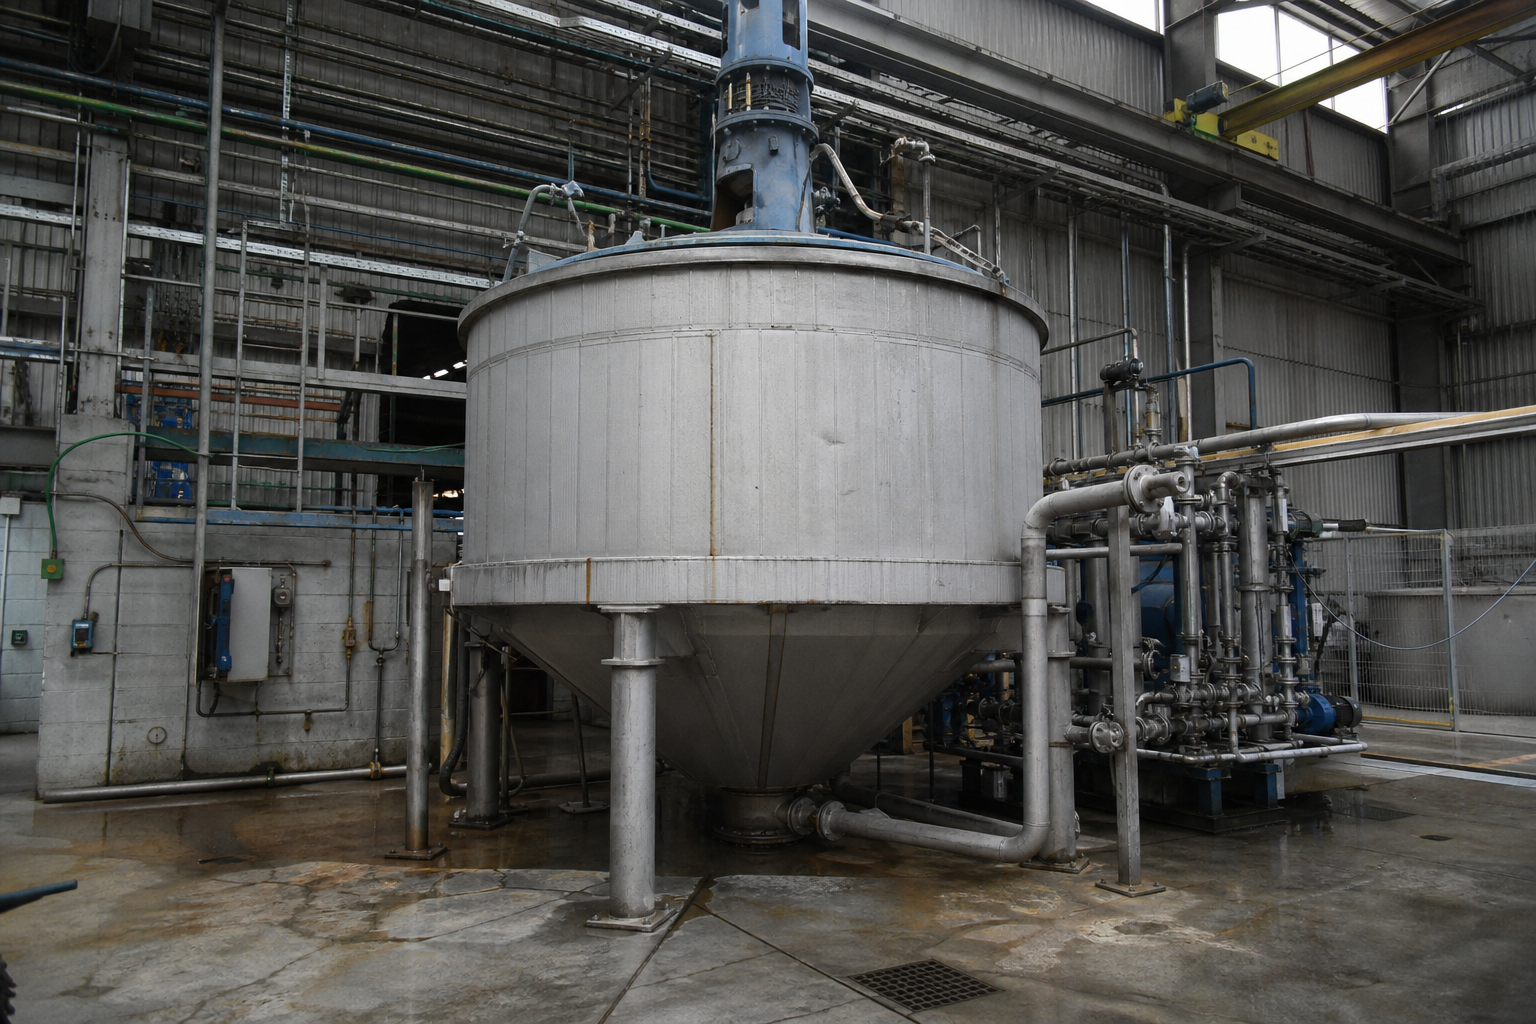
Industrial draft tube baffle DTB crystallizer vessel with top agitator
Technology

DTB Crystallizer: Principle and Application

DTB (draft-tube-baffle) crystallizers grow 1.0-3.0 mm uniform crystals with CV under 20% at 10-30% lower energy than forced circulation. Components, six-step cycle, the three parameters that set quality, a chlor-alkali
Read More »
Technical Specifications

DTB Crystallizer System Envelope — Published Supplier Data

Indicative ranges aggregated from published supplier specifications of draft-tube-baffle crystallizer builders (fertilizer, food and chemical executions). For route screening only — not a process guarantee for any specific project.

System SectionParameterPublished Indicative RangeApplies To / Basis
Product crystalPSD window0.5–2.0 mm band · published DTB executions 600–1,200 μmclassified-fines removal keeps the distribution narrow
Internal circulationDraft-tube velocity1–2 m/simpeller-driven upflow sets the growth-zone environment
Classification fieldBaffle-annulus velocity0.5–1 m/sthe elutriation cut — fines leave with the overflow, product crystals stay
Supersaturation controlOperating principleheld inside the metastable zoneinternal recirculation + external heat exchange prevents spontaneous nucleation
Fines removalElutriation circuitsettling-zone overflow carries fines to a dissolution loopdedicated fines-elimination device published on DTB executions
Crystal slurrySlurry-density band15–30 wt%a primary operating lever on crystal size and PSD
Operation modesDutycontinuous (principal form) and batch executionspublished DTB product ranges
Route compatibilityDimension-C methodsvacuum-cooling · evaporative · direct-contact freezing · reactionall four published on DTB bodies
Scale-up basisDesign methodscaled on measured crystallization kinetics toward the target crystal sizepublished DTB design methodology

Ranges aggregate published specifications from draft-tube-baffle crystallizer builders. Figures are supplier-published indicative values for screening; a project number requires crystallization kinetics on your liquor and the target PSD specification.

Main Process Modules

The Train, Module by Module

Each module is selected on feed chemistry and duty — the envelope column gives published operating ranges per module type, not a single-project specification.

ModuleEquipment TypesSelection BasisIndicative Operating Envelope
Feed conditioningPolished liquor + preheatstable feed conditions protect the classified populationfeed density held through the effect train
Supersaturation generationVacuum-cooling · evaporative · freeze · reaction headDimension C choice per solubility curvevacuum-cooling: 2,000–4,000 Pa(abs) · 30–35 °C final · 1.5–2.0 h residence
Internal circulationImpeller + draft tubemixed suspension, growth-dominated population1–2 m/s draft-tube upflow
ClassificationBaffle annulus + settling zonenarrow PSD — fines out, product stays0.5–1 m/s gap velocity · fines leave with the mother-liquor overflow
Fines dissolutionExternal fines-destruction loopredissolved fines recycle as growth inventorydedicated device published on DTB executions
Heat exchangeExternal exchanger on the recirculation looplow ΔT suppresses wall nucleationcleanable, slurry-class execution
Solid–liquid separationPeeler / pusher centrifugedewatering a 15–30 wt% slurry of narrow-PSD crystalscoarse narrow PSD dewaters sharply
Washing & dryingFluidized-bed dryer + screeningmoisture and grade controlnarrow PSD dries uniformly

Module envelopes follow the published supplier data above; draft-tube velocity, baffle cut and fines-dissolution rate are project-specific and set at design.

DTB Crystallizers in the Field — Case Studies & Technical Guides

Industrial draft tube baffle DTB crystallizer vessel with top agitator
Technology

DTB Crystallizer: Principle and Application

DTB (draft-tube-baffle) crystallizers grow 1.0-3.0 mm uniform crystals with CV under 20% at 10-30% lower energy than forced circulation. Components, six-step cycle, the three parameters that set quality, a chlor-alkali

Read More »
Positioning & Evidence

DTB is a Dimension D crystal growth configuration — the selection logic is explicit: product quality first, with stable crystal size, easy centrifugation and minimal mother-liquor carryover. It pairs with any Dimension C supersaturation method (evaporative, cooling, vacuum cooling). d50 and PSD outcomes depend on residence time, fines-management settings, slurry density (15–30 wt% band) and the driving-force profile. All figures are indicative ranges for preliminary screening, not a process guarantee.

FAQ · Engineering Answers

DTB Crystallizer Questions We Answer Most

Recurring questions from engineers choosing a growth configuration.

QWhat does the baffle actually do?

It creates a low-velocity annulus (0.5–1 m/s) where fine crystals are elutriated out of the growth zone, dissolved and recycled. Removing fines continuously is what keeps the product distribution narrow — without it, the fines compete for solute and the PSD widens.

QHow do I choose between DTB and Oslo for high-purity crystals?

DTB delivers 0.5–2 mm with classified-fines removal — preferred when downstream centrifugation throughput is the priority. Oslo produces larger crystals (1–5 mm) with very low fines — preferred when crystal size and purity matter most. Both reach high purity; the choice depends on which downstream property you value.

QCan DTB handle scaling feeds?

Good but not FC-grade. DTB tolerates moderate scaling tendency; on high-TDS, heavily scaling mixed-salt liquors, FC's high-velocity loop is the reliable choice. Putting classified equipment on an unstable feed trades availability for PSD you may never collect.

QWhat does slurry density control buy me?

The 15–30 wt% band is a primary size lever — higher slurry density gives more crystal surface area, lower per-crystal supersaturation and larger product. It is one of the main operating variables, tuned against the fines-removal rate.

Screening a DTB Configuration?

Send us the chemical system, target PSD and purity, and feed conditions. We will return a preliminary DTB vs. FC vs. Oslo screening with indicative crystal size — not a brochure.

Request a Proposal

Send your feed characterization (TDS, COD, main salts, viscosity), throughput and product targets — we respond with a preliminary process route within two business days.