
EvapCryst logo

Oslo — Fluidized-Bed Crystallizer

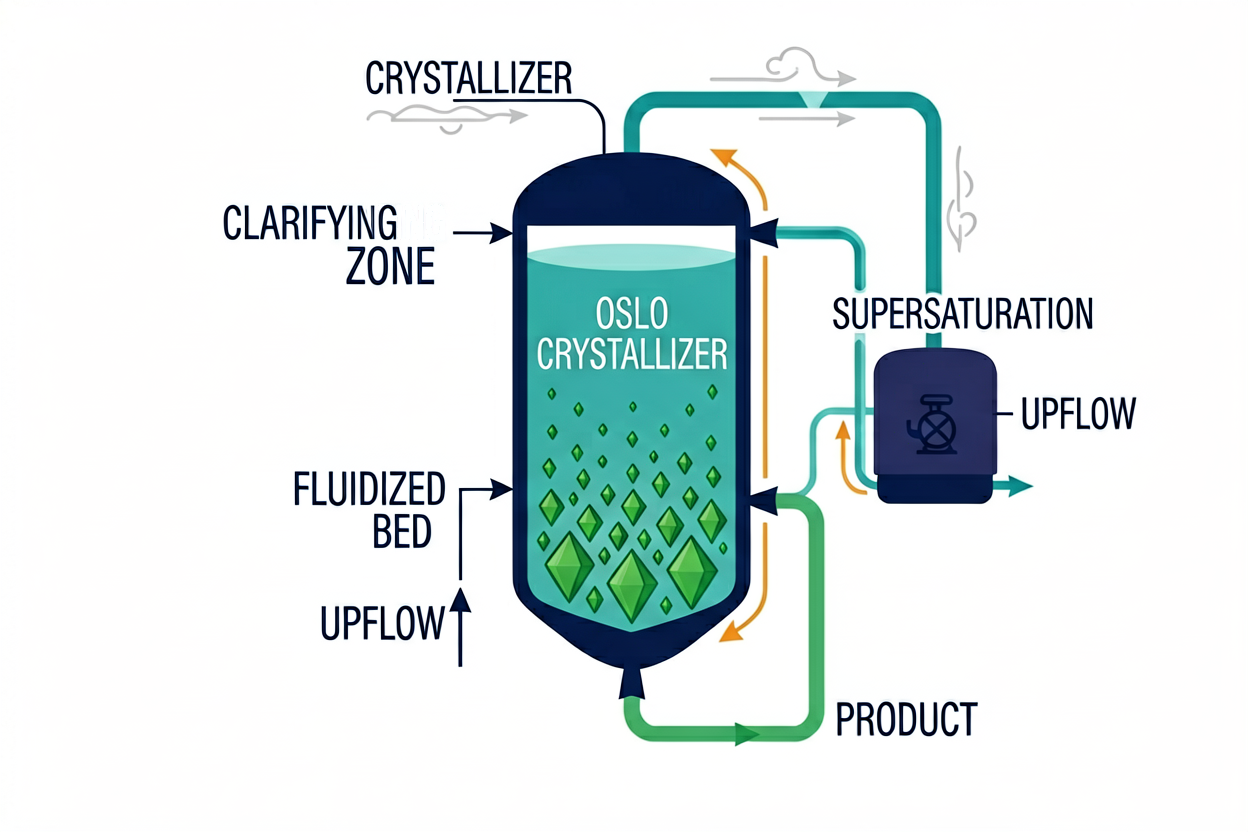
Crystal quality first. Supersaturated liquor flows up through a fluidized bed of crystals at very low velocity; crystals grow slowly in suspension and classify themselves by size. The largest crystals of any configuration — 1–5 mm, very uniform — earned on feeds with verified stability.

Oslo type crystallizer for large crystal production
At a Glance

Four Numbers That Define Oslo

Reference ranges under typical operating conditions on inorganic salt systems.

Crystal Size (d50)
1.0–5.0 mm
large, very uniform — the largest product of any standard configuration, classified naturally by fluidization
Fluidization Velocity
0.02–0.05 m/s
extremely low upward velocity through the bed — the crystals stay suspended in a gentle classification field
Supersaturation Limit
≤1–2 g/L
sub-metastable zone throughout the bed — exceeding it triggers spontaneous nucleation, fines and bed cementation
Crystal Residence Time
Long
hours to tens of hours — the price and the mechanism of large-crystal growth
Working Principle

Grow Slowly in a Suspended Bed

Supersaturation is generated externally and fed gently through the bed; the crystal population grades itself from fines at the top to product at the bottom.

Simplified Oslo Flow Diagram

Liquor → External supersaturation generation (Dimension C method) → Upflow through fluidized crystal bed (0.02–0.05 m/s) → Classified growth → Large product drawn from bed bottom → Clarified mother liquor overhead

The bed is the classifier: small crystals ride high, grown crystals sink to the discharge zone — no mechanical classification hardware.

01

External Supersaturation

The driving force is generated outside the bed — by evaporation or cooling per the plant's Dimension C method — and kept at ≤1–2 g/L.

02

Fluidized Bed

Liquor rises through the bed at 0.02–0.05 m/s; crystals remain suspended and grade by size.

03

Slow Classified Growth

Crystals spend hours to tens of hours in the bed, growing large and uniform with very low fines.

04

Classified Discharge

The largest crystals concentrate at the bottom of the bed and are drawn off as product; clarified liquor leaves overhead.

The Hard Constraint

Why Supersaturation Must Stay at ≤1–2 g/L

The fluidized bed holds the entire crystal population inside the metastable zone — that single constraint explains both what Oslo delivers and what it cannot tolerate.

ConditionWhat happens in the bed
Driving force ≤1–2 g/LAll growth occurs on existing bed crystals — large, uniform product with very low fines
Driving force above ~1–2 g/LSpontaneous nucleation fires inside the bed: new fines appear, classification degrades, and the bed can cement
Unstable or fouling-prone feedFeed excursions spike supersaturation — Oslo earns its higher CapEx only on feeds with verified stability

This is why Oslo is specified for value-bearing, well-characterized systems — battery-grade sulfates, electronic-grade salts — and not for uncertain liquors: the failure mode is structural, not gradual.

Configuration Selection

FC vs. DTB vs. Oslo

Three vessel configurations, three priorities: FC puts engineering reliability first, DTB puts product quality first, Oslo puts crystal quality first.

ParameterFCDTBOslo (this page)
Selection priorityEngineering reliabilityProduct quality (narrow PSD)Crystal quality (large, pure)
Typical crystal size0.2–0.8 mm — moderate, wide distribution0.5–2.0 mm — larger, controlled1.0–5.0 mm — large, very uniform
Fines removalNone standard — no internal classificationYes — classified-fines removal loop (elutriation zone)Natural — classification by fluidization
Circulation velocity2–3 m/s external loop1–2 m/s internal draft tube0.02–0.05 m/s fluidization upward velocity
Supersaturation toleranceHigh — recirculation dilutesMedium — controlled by draft-tube velocityLow — ≤1–2 g/L to avoid spontaneous nucleation
Best forHigh-salinity, scaling-prone, mixed-salt systems: NaCl, Na₂SO₄, ZLD mixed saltsFertilizer (NH₄)₂SO₄, KCl, battery-grade Li₂CO₃ precursor, organic acidsBattery-grade NiSO₄ / CoSO₄ / MnSO₄, pharma intermediates, electronic-grade salts
Residence timeMedium (hours)Medium (hours)Long (tens of hours)

d50 ranges reflect typical operating distributions on inorganic salt systems; actual PSD depends on residence time, bed management and the driving-force profile.

Selection

When to Pick Oslo — and When Not To

Oslo is the answer when large, high-purity crystals justify higher CapEx, long residence and a verified-stable feed; the wrong answer on uncertain liquors.

Technical Specifications

Oslo Crystallizer System Envelope — Published Supplier Data

Indicative ranges aggregated from published supplier specifications of Oslo fluidized-bed crystallizer builders (inorganic-salt and value-salt executions). For route screening only — not a process guarantee for any specific project.

System SectionParameterPublished Indicative RangeApplies To / Basis
Product crystalPSD window1–5 mm classified-bed productthe largest crystals of any standard configuration — the bed grades itself
Bed hydraulicsFluidization velocity0.02–0.05 m/s upflowgentle classification field; no mechanical classifying internals
Supersaturation controlBed limit≤1–2 g/L sub-metastable through the bedexceeding it triggers spontaneous nucleation, fines and bed cementation
Supersaturation controlControl leverscirculation rate · temperature · evaporation ratepublished Oslo operating variables — too high bursts nucleation, too low stalls growth
Zone architectureTwo-zone designsupersaturation generated in a separate zone; growth in the fluidized bedcentral downcomer + bottom-up flow through the classified bed
Product qualityDownstream benefitlarge, uniform crystals filter, wash and dry better — lower moisture, higher puritypublished Oslo product rationale
Operation modesDutycontinuous and batch executions · mother-liquor-circulation typepublished Oslo classifications
Scaling serviceHeat-surface protectioncleaning-liquor circulation on the exchanger looppublished practice to cut heat-surface scaling risk
Whole trainCapacity & energy (Oslo executions)0.5–2 t/h double-effect · 3–50 t/h triple-effect · MVR drive 15–40 kWh per t waterpublished salt lines select OSLO / FC / DTB bodies by salt species
On-streamCIP interval≥10–20 dayspublished salt-crystallizer CIP cycles; cleaning-liquor circulation protects the exchanger
Crystal residenceTime in bedlong — hours to tens of hoursthe price and the mechanism of large-crystal growth

Ranges aggregate published specifications from Oslo fluidized-bed crystallizer builders. Figures are supplier-published indicative values for screening; a project number requires solubility data, liquor clarity and the crystal-size target that justifies the classified bed.

Main Process Modules

The Train, Module by Module

Each module is selected on feed chemistry and duty — the envelope column gives published operating ranges per module type, not a single-project specification.

ModuleEquipment TypesSelection BasisIndicative Operating Envelope
Feed conditioningClarified, solids-free liquorthe classified bed is intolerant of suspended feed solidsvalue-salt service polishes the feed
Supersaturation generationExternal zone — evaporative / vacuum-cooling / freezegeneration and growth kept apart≤1–2 g/L fed to the bed
Fluidized growth bedCentral downcomer + bottom-up classified bedcrystals grade from fines (top) to product (bottom)0.02–0.05 m/s upflow
ClassificationThe bed itself — hydraulic, no internalsproduct drawn from the bottom zone1–5 mm product window
Mother-liquor circulationClarified overflow returns through the generation zonemother-liquor-circulation architecturepublished Oslo type designation
Heat exchangeExternal exchanger with cleaning-liquor circulationscale control on the generation looppublished anti-scaling practice
Separation & dryingCoarse-product centrifuge + dryerlarge uniform crystals wash and dewater efficientlylow final moisture on uniform product

Module envelopes follow the published supplier data above; fluidization velocity, bed height and supersaturation feed rate are project-specific and set at design.

Positioning & Evidence

Oslo is a Dimension D crystal growth configuration, pairing with any Dimension C supersaturation method that can deliver its output gently and at ≤1–2 g/L driving force. The selection logic is explicit: crystal quality first — large particles, narrow distribution — with the acknowledged costs of higher CapEx, long crystal residence and sensitivity to feed stability. All figures are indicative ranges for preliminary screening, not a process guarantee.

FAQ · Engineering Answers

Oslo Crystallizer Questions We Answer Most

Recurring questions from engineers choosing a growth configuration.

QWhy does Oslo need such low supersaturation — ≤1–2 g/L?

The fluidized bed holds the entire crystal population inside the metastable zone. Above roughly 1–2 g/L of driving force, spontaneous nucleation fires inside the bed: new fines appear, the classification that produces those 1–5 mm crystals degrades, and the bed can cement.

QWhy does Oslo cost more than FC or DTB?

Long crystal residence means a large vessel per tonne of product, and the feed must be characterized well enough to hold the sub-metastable driving force continuously. You pay for size and certainty — which is why the configuration pencils out on value-bearing salts.

QCan Oslo handle wastewater ZLD duty?

Not usually. ZLD mixed-salt brines are scaling-prone and composition-variable — exactly the feed instability Oslo cannot tolerate. FC bodies carry that duty; Oslo is reserved for product crystallization on stable liquors.

QHow do I choose between Oslo and DTB for battery-grade sulfates?

Both reach battery-grade purity. Oslo delivers 1–5 mm with very low fines and long residence; DTB delivers 0.5–2 mm with classified-fines removal at higher throughput per vessel. If crystal size and downstream handling of large crystals dominate, Oslo; if capacity and centrifuge throughput dominate, DTB.

Oslo Crystallizers in the Field — Case Studies & Technical Guides

Tall Oslo growth crystallizer vessel in an industrial plant
Technology

Oslo Crystallizer: Principle and Application

Oslo (fluidized-bed / Krystal) crystallizers decouple supersaturation generation from crystal growth to deliver 2-5 mm crystals, CV under 5%, and impurities below 0.1%. Structure, countercurrent mechanism, evaporative vs cooling variants,
Read More »

Screening an Oslo Configuration?

Send us the chemical system, solubility data, target PSD and purity. We will return a preliminary Oslo vs. DTB vs. FC screening with indicative crystal size — not a brochure.

Request a Proposal

Send your feed characterization (TDS, COD, main salts, viscosity), throughput and product targets — we respond with a preliminary process route within two business days.