Project Parameters
| Parameter | Value |
|---|---|
| Process route | MVR evaporation + forced-circulation crystallization |
| Industry | Battery materials — cobalt tetroxide (Co3O4) precursor production (Central China) |
| Feed type & key components | Ammonium chloride wastewater from cobalt precipitation; NH4Cl-dominant brine with trace cobalt values |
| Evaporation capacity | 33 t/h |
| Construction materials | SS316L wetted parts (indicative for chloride service; higher alloys in the hottest zones) |
Representative process configuration compiled from published industry project data. Indicative values, not a process guarantee.
Project Description
Cobalt tetroxide, the precursor that becomes lithium cobalt oxide inside nearly every phone and laptop battery, is precipitated from cobalt salt solutions with alkali and ammonium reagents — and the counter-ion leaves the process as ammonium chloride wastewater. At a cobalt precursor plant in Central China, this stream arrives continuously at a scale of 33 t/h: a single-salt brine that cannot be discharged at concentration but carries a salt with real product value, since ammonium chloride trades as fertilizer grade and as a battery-materials precursor input. The treatment objective is therefore recovery, not disposal: evaporate the water, crystallize the salt, return the condensate.
Two engineering realities define the plant. Ammonium chloride brine is chloride service — wetted materials are selected for chloride corrosion at temperature, with SS316L as the indicative reference grade and higher alloys where concentration and temperature peak. And ammonium chemistry is volatile-adjacent: the system must be sealed and pH-controlled to keep the ammonia in the product and out of the condensate and plant air. Trace cobalt that escapes the precipitation section is worth polishing out upstream of the evaporator — it is product value, and it contaminates the salt if it passes through.
Process Technology
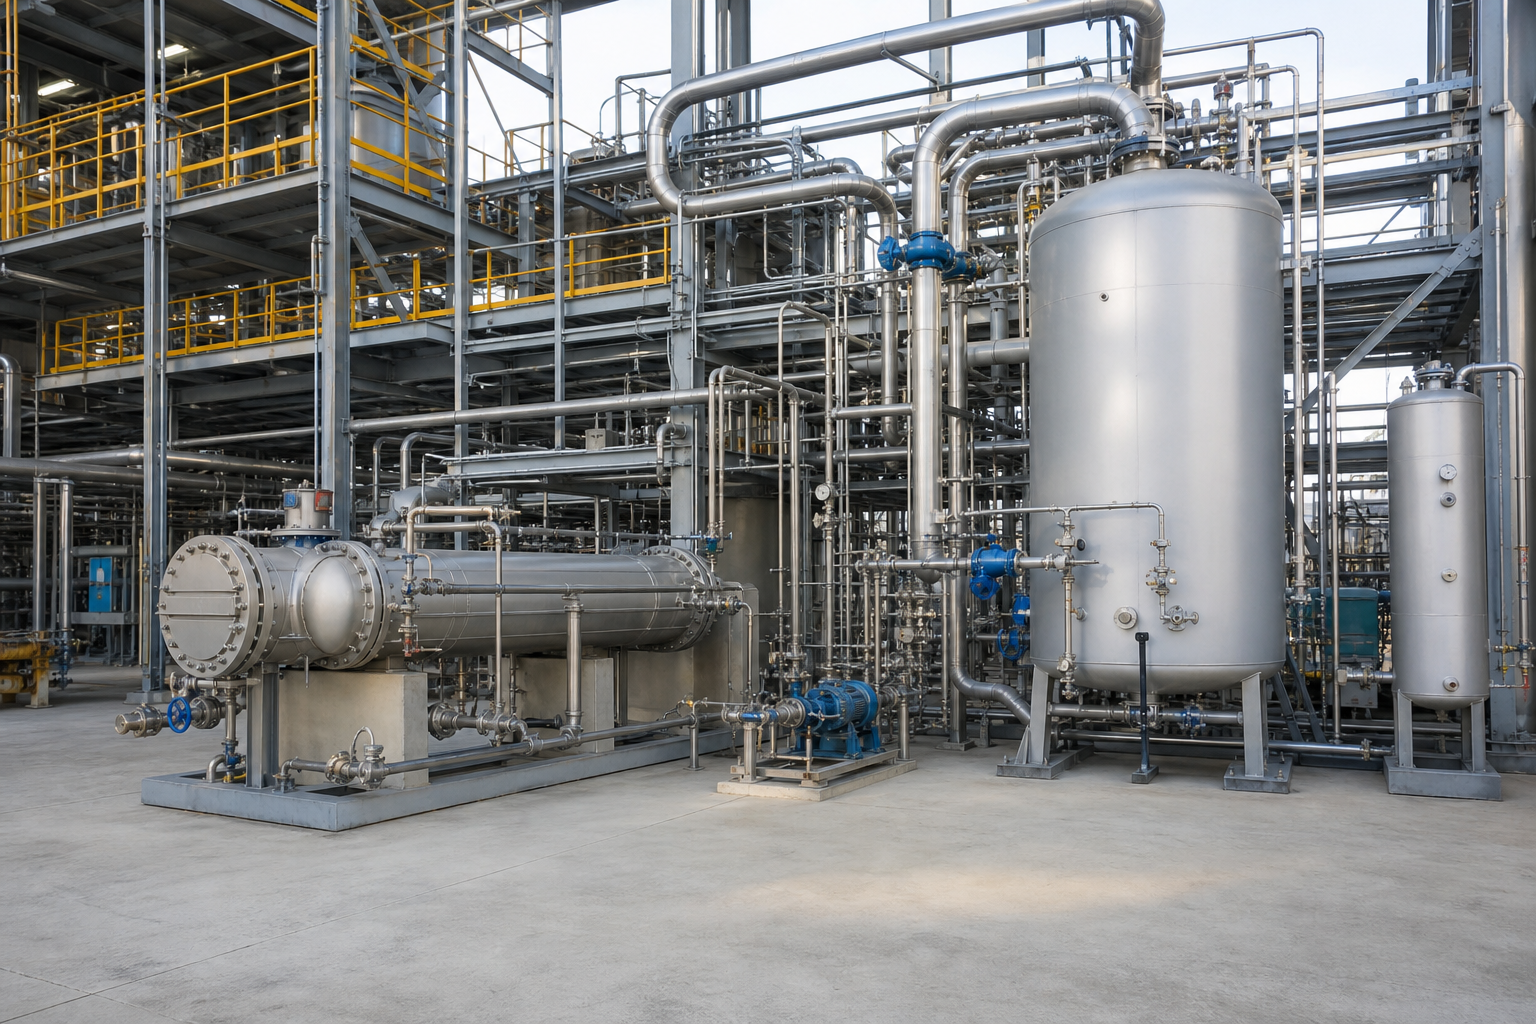
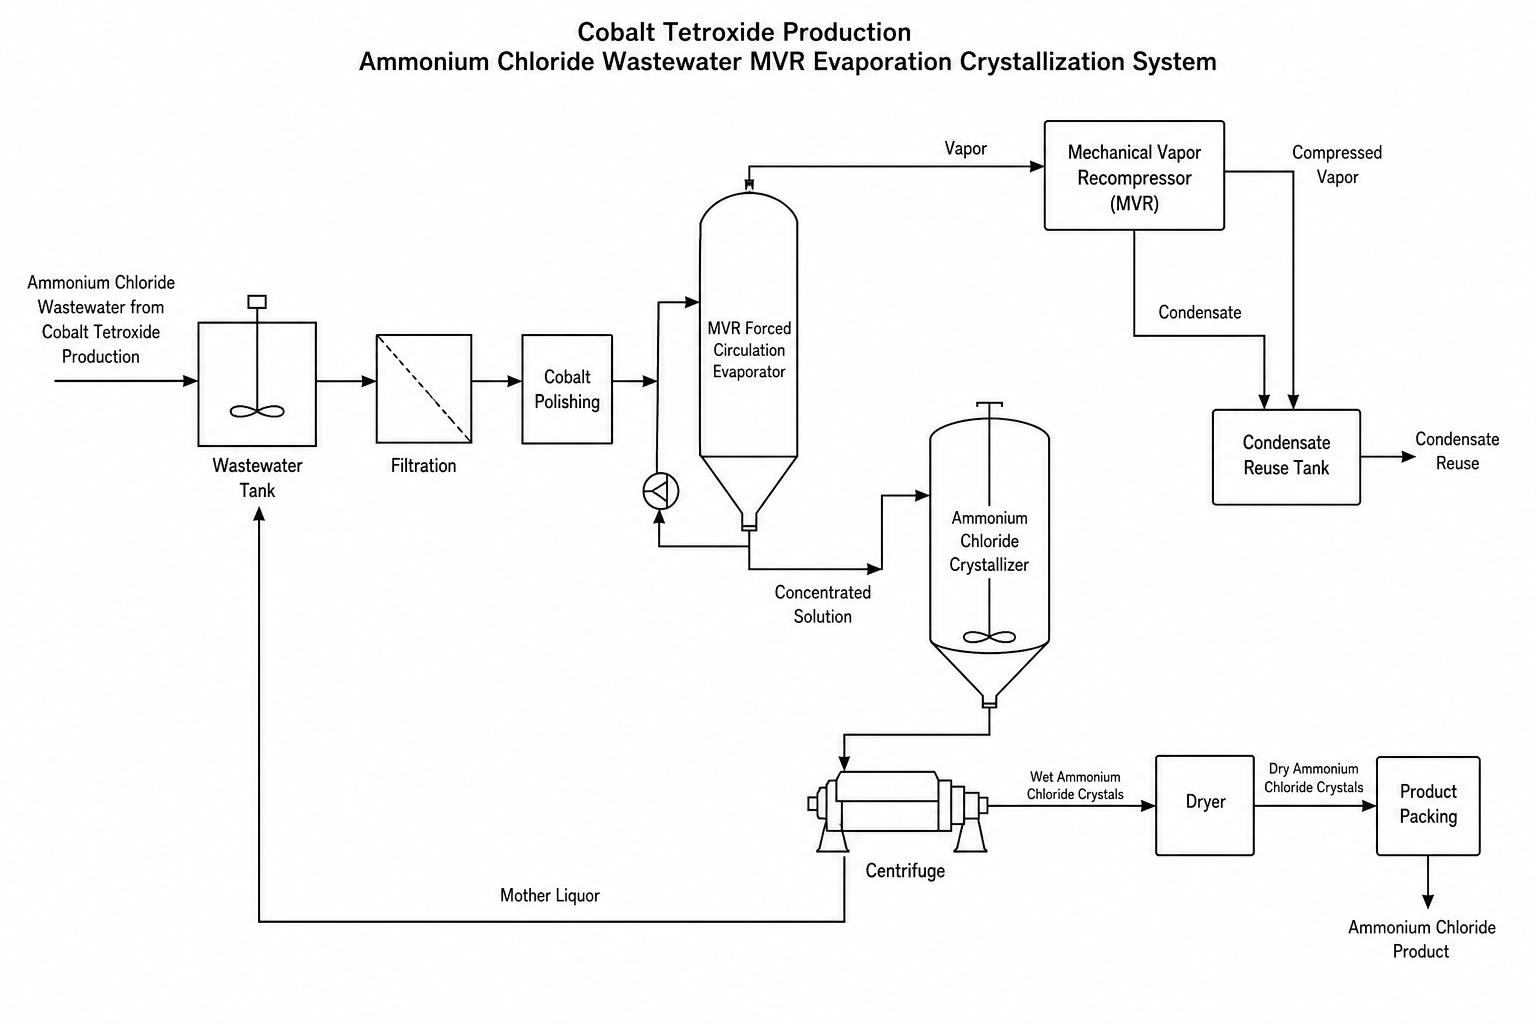
The wastewater is equalized and filtered for suspended solids, and a polishing step recovers residual cobalt values before the thermal section — both for the metal value and for the purity of the ammonium chloride product.
Concentration runs on MVR evaporation. The mechanical vapor recompressor takes the secondary vapor from the separator, raises its pressure and temperature electrically, and returns it to the heater as the driving steam — the plant runs on electricity rather than live steam, which is the decisive economics for a salt-recovery duty where steam would be the largest operating cost. As the liquor approaches NH4Cl saturation the duty transitions to forced-circulation crystallization — the standard regime for a crystallizing chloride salt, where pumped velocity keeps the heat transfer surface clean and supersaturation is relieved on growing crystals rather than on the exchanger wall.
The crystallizer grows ammonium chloride under controlled slurry density, with pH management pinning the ammonia equilibrium to the liquid phase. Centrifuging dewaters the crystal slurry; a dryer finishes the salt to product moisture for fertilizer or industrial offtake. Mother liquor recycles to the evaporator feed with a small purge controlling trace species, and condensate — the majority of the 33 t/h by mass — is collected hot and clean for reuse as process water in the precursor plant.
Comparable published configurations in the same cobalt segment include a four-line cobalt precursor plant treating 1,220 m³/d of ammonium chloride wastewater, confirming the evaporation-crystallization route across the segment’s capacity range.
Equipment Configuration
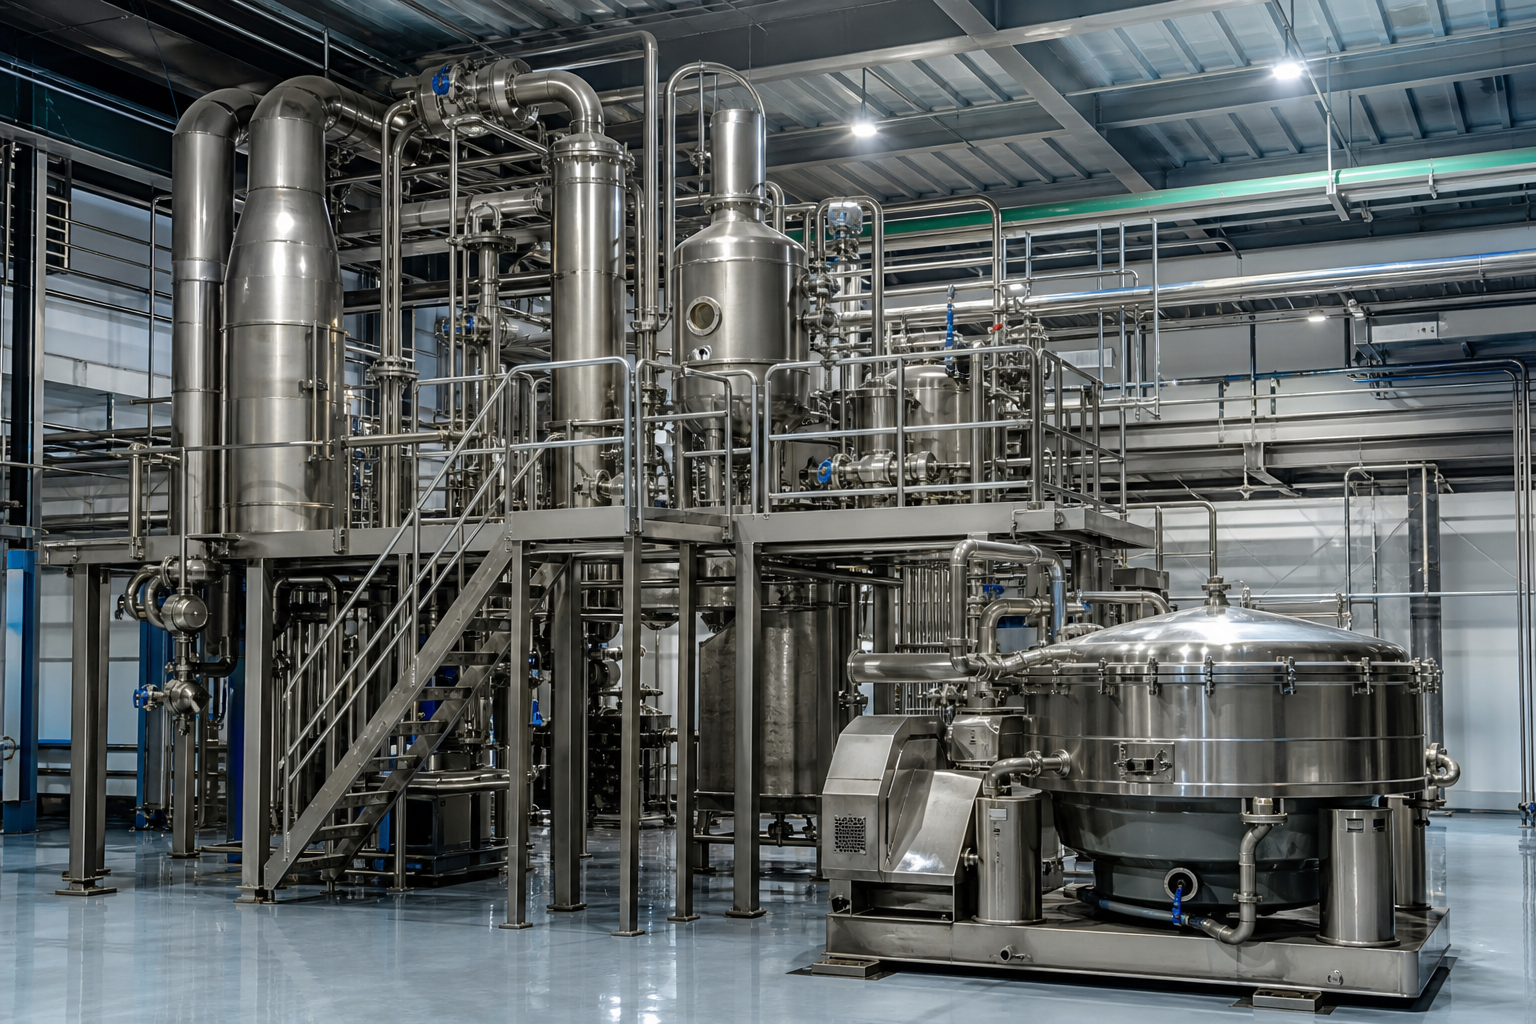
One set of the following equipment is typical for this duty:
- Feed equalization, filtration and trace cobalt polishing
- MVR forced-circulation evaporator-crystallizer with centrifugal vapor recompressor
- Crystallizer section with pH-controlled ammonia management
- Centrifuge and dryer finishing product-grade ammonium chloride
- Mother-liquor return and purge; condensate recovery for plant reuse
- PLC/DCS control of density, compressor operation and crystal inventory
Performance & Outcome
Compiled from published industry project data, indicative: trains of this class convert cobalt-line ammonium chloride wastewater into product-grade NH4Cl on electrically driven MVR energy, with condensate recovered as process water. Salt purity and specific energy are quoted per project brine chemistry.