Project Parameters
| Parameter | Value |
|---|---|
| Process route | MVR forced-circulation evaporation + crystallization |
| Industry | Rare earth separation and processing |
| Feed type & key components | High-sodium-salt wastewater from rare earth separation circuits (sodium salts dominating) |
| Throughput | 100 t/d feed treatment (published as processing capacity) |
| Construction materials | SS316L / duplex (indicative) |
Representative process configuration compiled from published industry project data. Indicative values, not a process guarantee.
Project Description
A rare earth separation plant in Chongzuo, Guangxi, Southwest China, sits at the midstream of the rare earth chain: concentrated feedstock is dissolved, separated by solvent extraction into individual rare earths, and precipitated as carbonates and oxides. Each precipitation step consumes sodium carbonate or sodium hydroxide and each acid wash leaves sodium behind, so the site’s wastewater is dominated not by the valuable rare earths — those are recovered upstream — but by sodium salts at concentrations that bar discharge under the karst region’s strict water protection regime. The published duty is a 100 t/d processing capacity evaporation and crystallization system that closes the site’s salt balance.
The reference configuration is an MVR forced-circulation evaporation and crystallization package. For a separation plant whose sodium load arrives as mixed chloride and sulfate salts, forced circulation under mechanical vapor recompression gives the robust, electrically heated route to mixed-salt solids and recyclable water at continuous campaign duty.
Process Technology
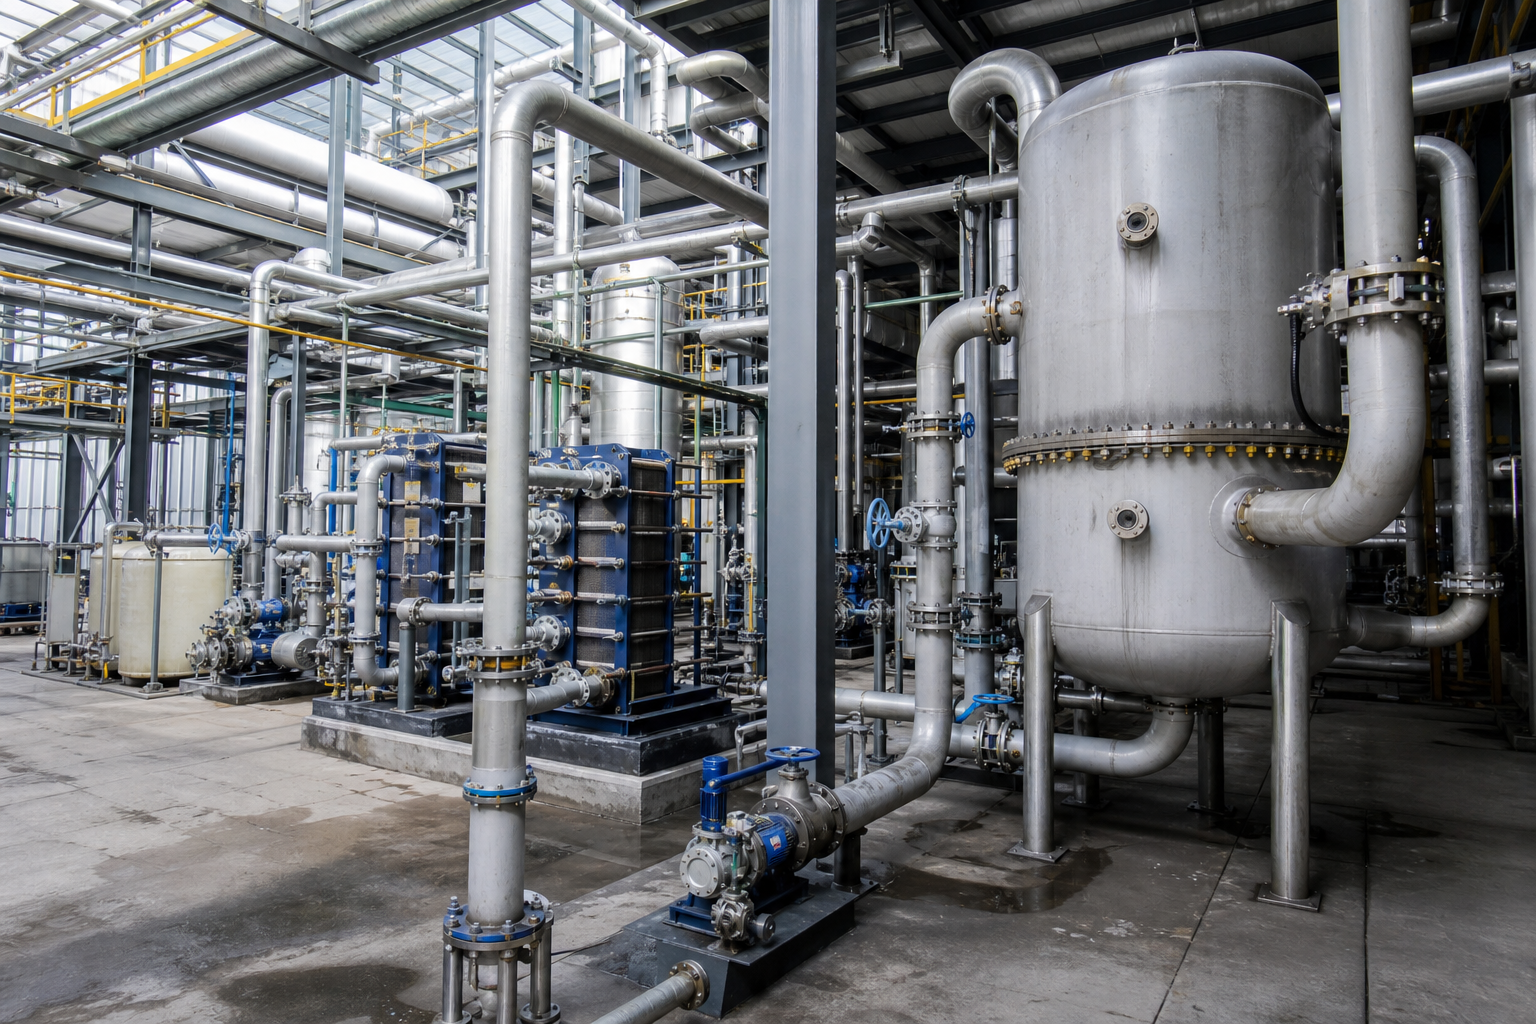
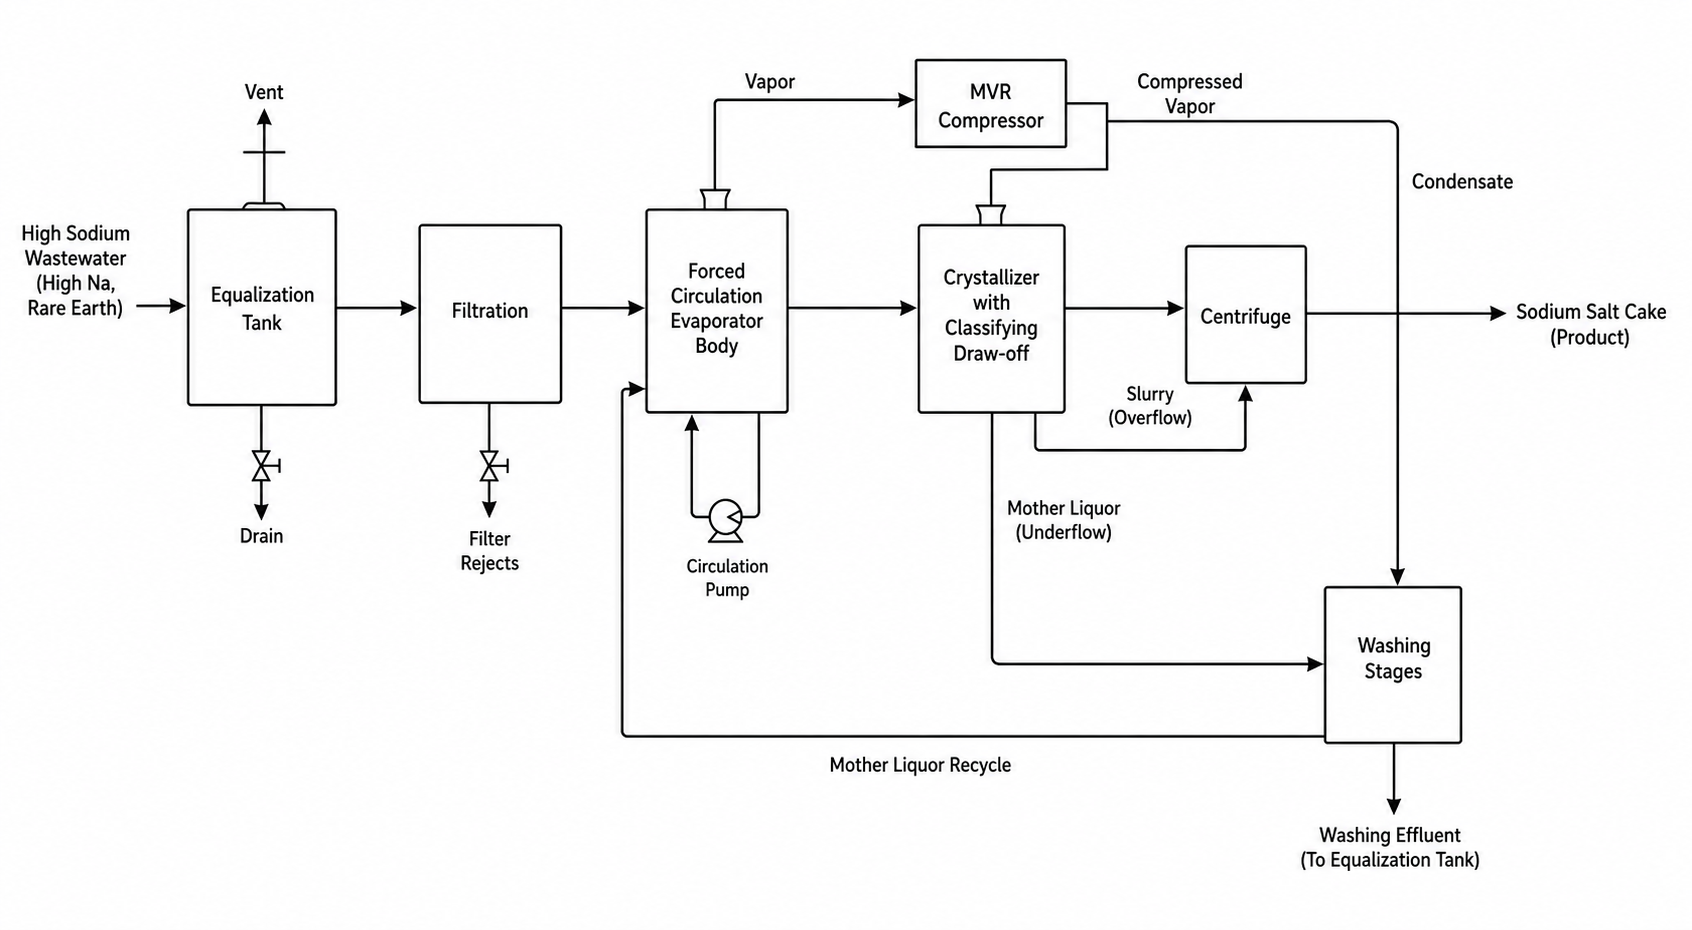
Wastewater is equalized in tanks that absorb the batch rhythm of the extraction and precipitation circuits, and residual rare earth values are recovered upstream of the train — the evaporation system receives a liquor whose metal content has already been scavenged, protecting both salt quality and the plant’s yield. The liquor is filtered and, where the sulfate-to-chloride balance requires it, conditioned toward the crystallization route the site has selected.
The train concentrates under MVR: forced-circulation loops pump the liquor through tubular heaters at high velocity with vapor release in flash separators, and the compressor lifts the separated vapor back to heating duty. Because the sodium salts crystallize as concentration proceeds, the salt is managed where it forms — suspension in the circulating loop, classifying draw-off to the crystallizer body, and dewatering on centrifuges. Mixed sodium salt cake leaves the system as a solid for compliant disposal or downstream salt refining; the mother liquor recycles with a purge controlling trace accumulation.
The water side is the quieter half of the balance sheet: condensate from the surface condenser is collected, checked, and returned to the separation plant’s washing and precipitation stages. In a region where water permits are as binding as discharge permits, recovering the majority of the wastewater as in-plant reuse water is worth as much as the salt management.
Equipment Configuration
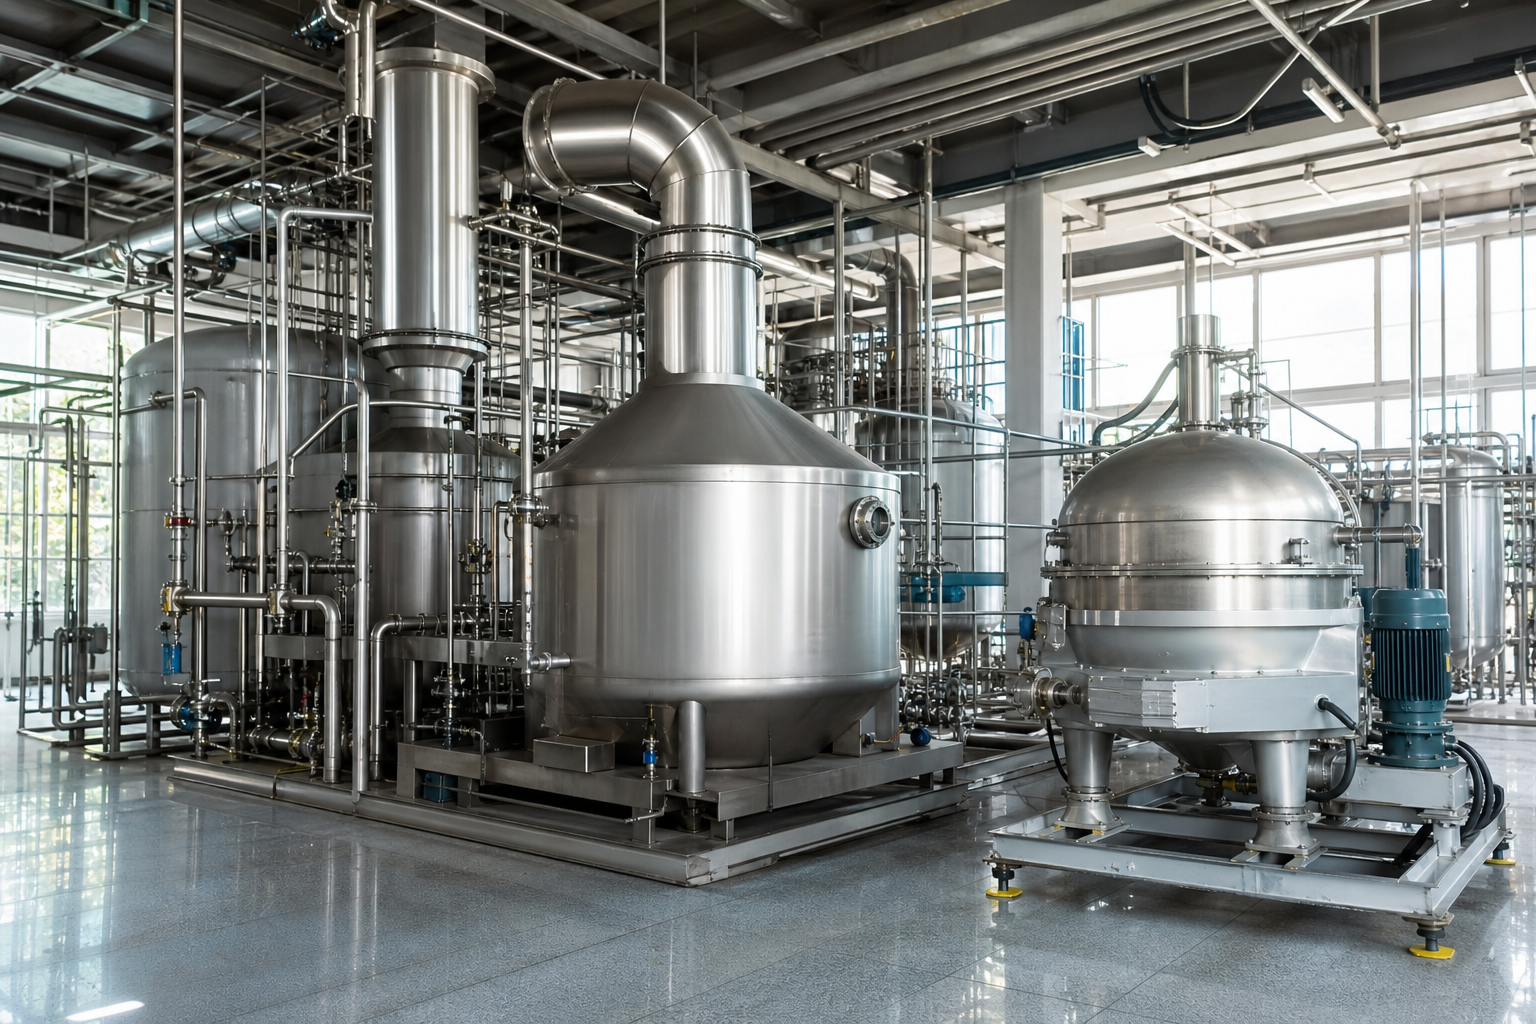
One system of this class comprises:
- Equalization and filtration with upstream rare earth scavenging interface
- MVR forced-circulation evaporator body with mechanical vapor recompressor
- Crystallizer with classifying draw-off; centrifuges for mixed sodium salt cake
- Mother-liquor recycle with controlled purge
- Surface condenser, condensate tank and reuse pumping to washing stages
- Density- and temperature-based control with CIP circuits
SS316L is the indicative baseline for the sodium salt service, with duplex where the chloride fraction of the salt mix runs high at the hot end.
Performance & Outcome
Compiled from published industry project data, indicative: MVR systems of this class treat high-sodium rare earth wastewater at published feed capacities around 100 t/d, converting the sodium load to dewaterable mixed-salt solids and returning the water fraction as plant reuse. Salt quality, recovery and power figures depend on the salt mix and are validated per project.