
In hydrometallurgical lithium battery recycling, MVR evaporation-crystallization does two jobs at once: it concentrates dilute leachate five-to-ten-fold (a published illustrative range) before metal recovery, and it runs the salt-separation train that turns wastewater into battery-grade nickel and cobalt sulfate crystals plus separable sodium sulfate, potassium chloride, and sodium chloride. A published South Korean project operates this configuration at 7.75 t/h on nickel solution and 1.3 t/h on cobalt solution — external industry references, not EvapCryst project records — and Chinese projects at 68 to 70 t/h show the same chemistry at twenty times the scale.
Where the Salt Load in Battery Recycling Comes From
Hydrometallurgical recycling of ternary (NCM) and LFP batteries begins with mechanical disassembly to liberate cathode and anode material, followed by acid leaching with sulfuric or hydrochloric acid dissolving Ni2+, Co2+, Mn2+, and Li+. The leachate arrives dilute and large in volume, and processing it dilute would inflate reagent and energy demand in every downstream step — precipitation, solvent extraction, electrowinning. Evaporation lifts metal ion concentration, typically reducing liquor volume to one-fifth or one-tenth of the original.
The salt burden grows through the flowsheet: sodium carbonate for lithium precipitation introduces sodium, neutralization introduces sulfate and chloride, and washing multiplies the water volume. By the time mother liquors and wash waters reach the effluent system, the plant carries a mixed sulfate-chloride brine with nickel, cobalt, manganese, and lithium dissolved in it — both a treatment obligation and, at modern metal prices, a recovery opportunity.
Job One: Concentrating the Leachate
Leachate concentration is straightforward thermal engineering with metallurgical constraints. The liquor is filtered to remove solids and pH-adjusted to prevent metal precipitation in the evaporator, then pumped over heated surfaces at 60-90 degrees Celsius where it evaporates as a thin film. Metal concentrations leave five to ten times higher than they entered. The condensate is recovered for leaching or rinsing reuse, closing a meaningful share of the water balance, and the concentrate moves to precipitation, solvent extraction, or electrowinning.
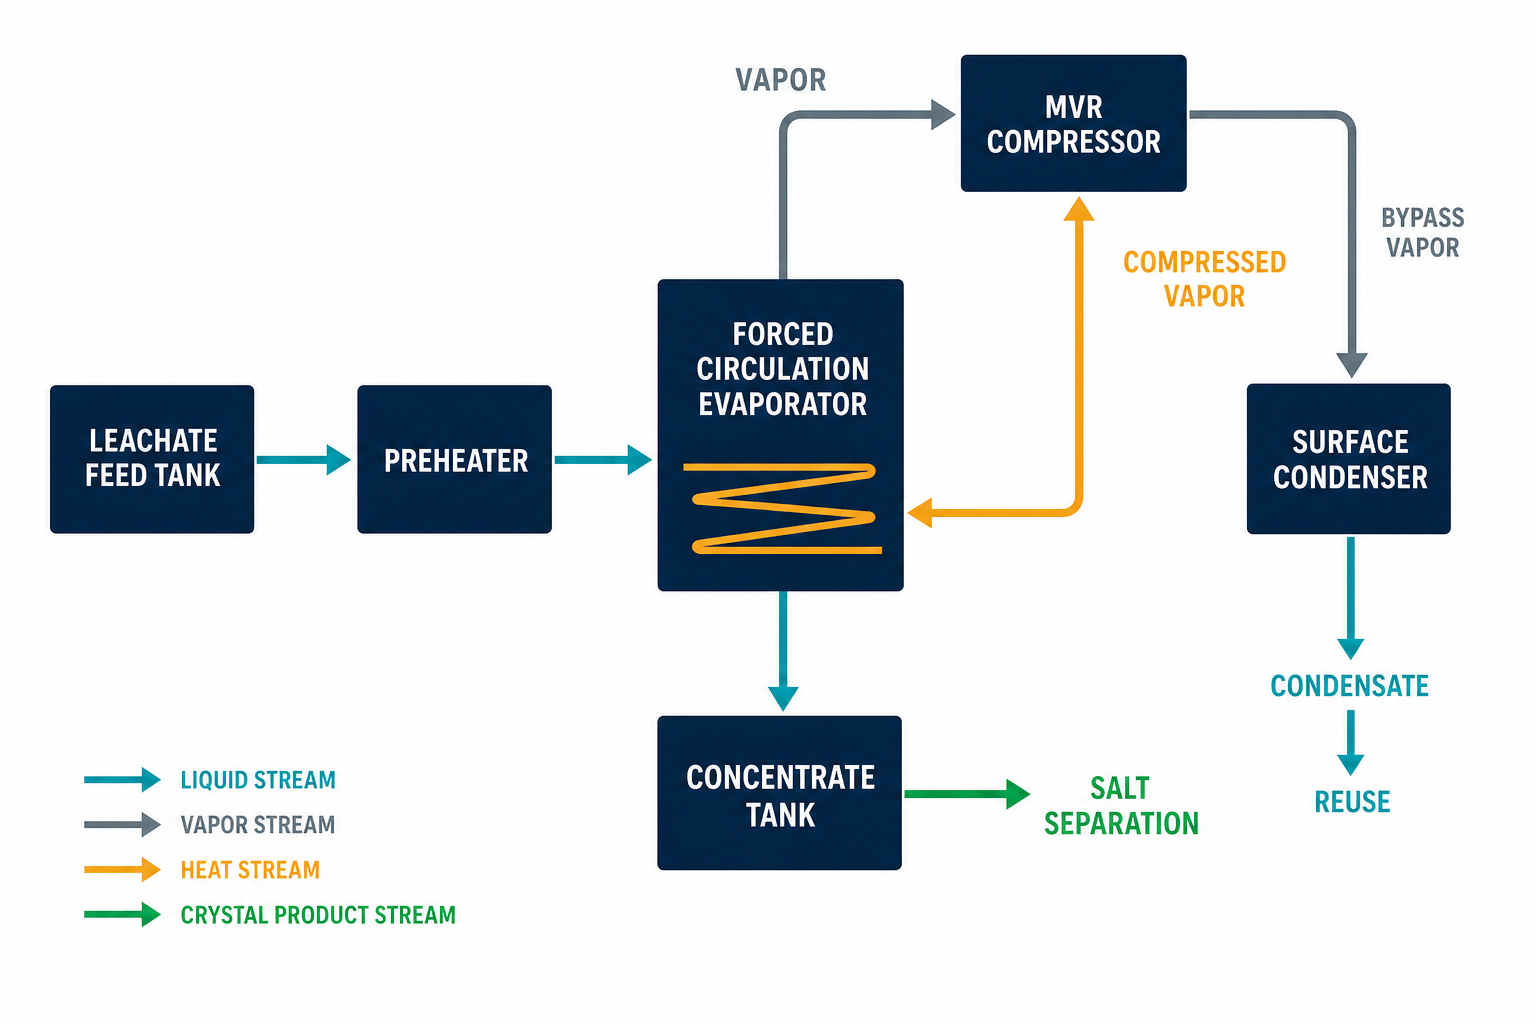
Two operating choices protect the metals: low-temperature vacuum evaporation avoids degrading heat-sensitive species and limits corrosion, and continuous self-cleaning operation reduces the fouling downtime that batch evaporation would impose on the recovery circuit.
Job Two: Salt Separation and Battery-Grade Crystal Production
The salt train is where recycling projects differentiate themselves. The published Korean configuration processes nickel- and cobalt-bearing solutions in parallel lines of forced-circulation evaporation followed by OSLO continuous freeze crystallization, producing NiSO4 and CoSO4 crystals to GB and JIS standards. The OSLO class matters for product value: its low supersaturation gradient and gentle fluidization grow large, uniform crystals — what battery-material buyers pay for.
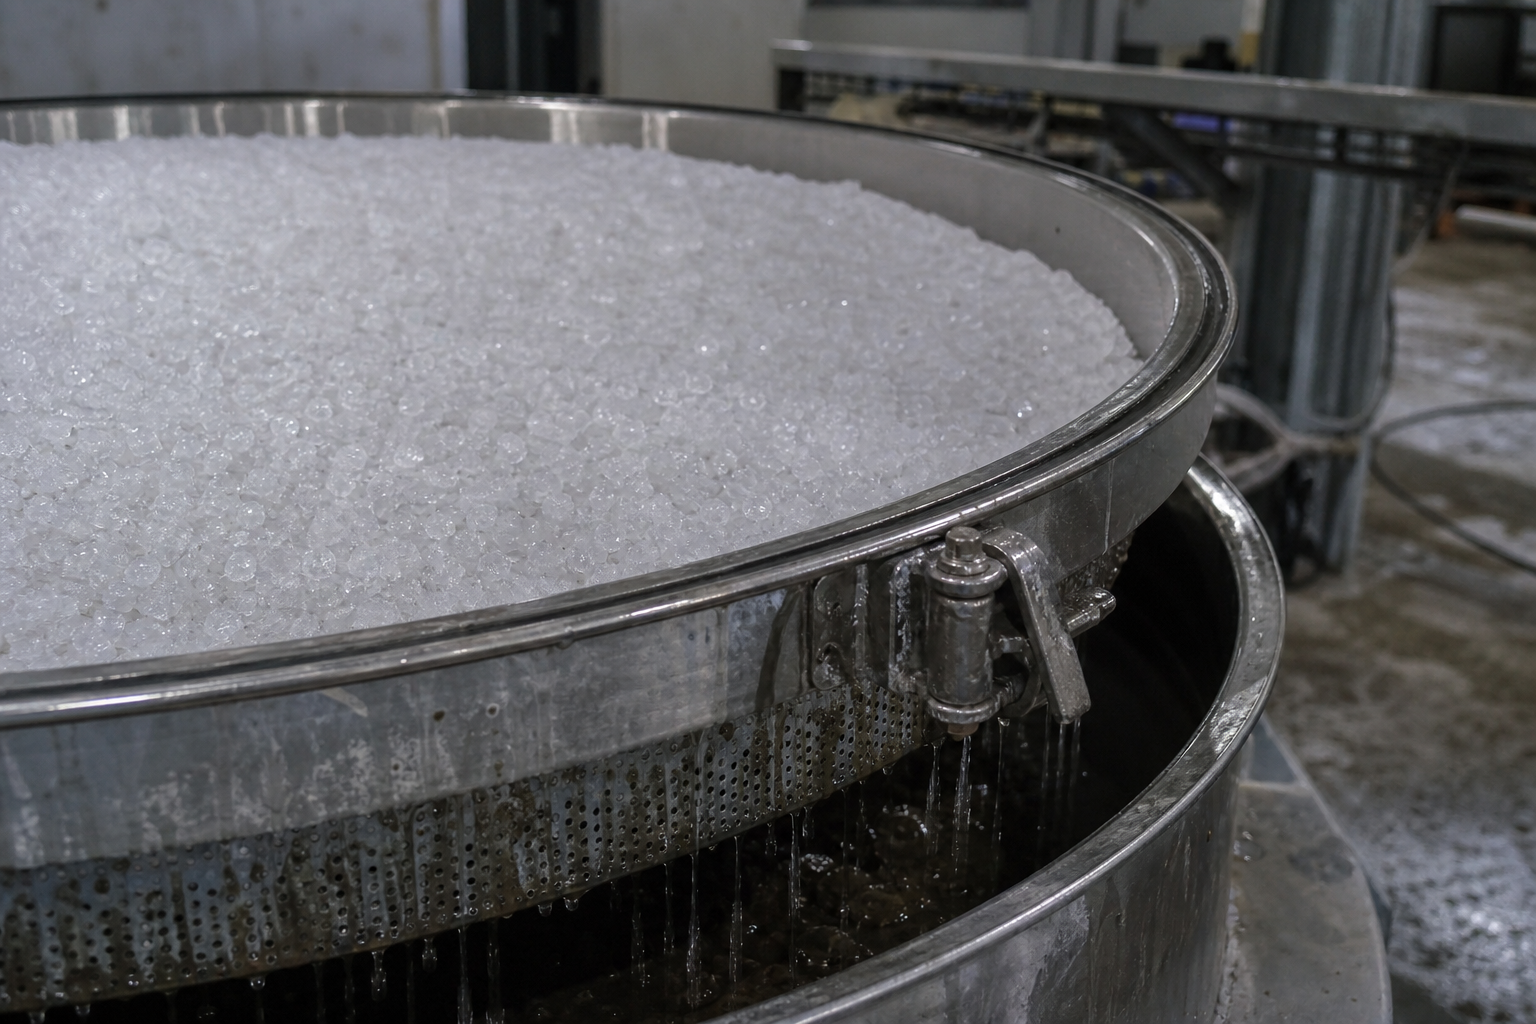
For the sodium-dominated waste salts, the separation logic sequences by solubility. Sodium sulfate is removed first, exploiting its steep retrograde solubility, then the lithium-bearing mother liquor advances through staged crystallization toward battery-grade lithium hydroxide or carbonate. Supplier documentation reports lithium product purity of 99.5-99.9% after cold washing and mother-liquor management, sodium chloride rejection above 99.5%, and metal recovery above 95% — indicative supplier-published figures, not project guarantees. At the four-salt extreme, published project scopes cover CoSO4, NiSO4, KCl, and NaCl separation from a single recycling effluent.
Reference Projects Across the Scale Range
| Project | Capacity | Products | Process notes |
|---|---|---|---|
| Hydrometallurgical recycling, South Korea | 7.75 t/h nickel line + 1.3 t/h cobalt line | NiSO4 and CoSO4 crystals | Forced-circulation evaporation + OSLO continuous freeze crystallization; GB & JIS flange standards |
| Iron phosphate (LFP) recycling, China | 70 t/h evaporation for a 100,000 tpa plant | Recovered battery-grade materials | MVR evaporation-crystallization |
| Iron phosphate (LFP) recycling, China | 68 t/h evaporation for a 50,000 tpa plant | Recovered battery-grade materials | MVR evaporation-crystallization |
| Four-salt separation project | Undisclosed | CoSO4, NiSO4, KCl, NaCl fractions | Evaporation with staged salt separation from recycling effluent |
The two LFP figures sit inside cathode-active-material production and recycling complexes: when the recycling economy scales toward 100,000 tonnes per year of feed, the evaporation duty scales with it into the 70 t/h class seen in commodity chemical brine plants. Evaporation is a process-scale unit operation here, not a niche utility.
Read by module, the published trains decompose as follows:
| Process module | Equipment candidates | Selection basis | Indicative envelope (published) |
|---|---|---|---|
| Leachate conditioning | Filtration, pH dosing | Prevent metal precipitation in the evaporator | Per solids and pH window |
| Leachate concentration | Low-temperature vacuum MVR evaporator | Lift metal concentration; protect heat-sensitive species | 60–90 °C; 5–10× concentration |
| Battery-grade crystallization | FC lines + OSLO freeze crystallization | Large uniform crystals for battery buyers | NiSO4 / CoSO4 to GB & JIS |
| Byproduct salt separation | Staged crystallization by solubility | Na2SO4 first (retrograde), then lithium route | NaCl rejection >99.5% (documented) |
| Mother-liquor management | Closed recycle with purge and cold wash | Yield versus impurity accumulation | Li purity 99.5–99.9% (supplier-reported) |
Configuration, materials, and operating ranges depend on the actual feed assay, corrosion review, product specification, utilities, and project capacity.
Energy and Economics: What Suppliers Report
MVR’s selling point in this application is the compression of energy cost per tonne of water evaporated. Supplier-published figures for MVR evaporation-crystallization on lithium brines run at roughly 40-60 kWh per tonne of water evaporated, with 50-80% energy reduction versus steam-driven alternatives and operating temperatures of 50-70 degrees Celsius under vacuum. One supplier documents payback on a lithium recovery installation shortening from three projected years to fourteen months once vapor recycling displaced steam ejectors — vendor-reported and site-specific, but the direction is consistent: MVR replaces purchased steam and the condensate displaces fresh water.
The counterweights are real: MVR carries higher initial investment than thermal alternatives, and the compressor is a rotating machine with maintenance needs. The economics clear when electricity is reasonably priced, the stream is large and steady, and the salts carry value — all three hold in battery recycling.
Purity Discipline: Battery-Grade Is a Moving Target
Selling recovered salts into cathode production means hitting battery-grade specs on sodium, calcium, iron, and magnetic impurities, not just the primary metal. The toolkit around the crystallizers includes impurity precipitation ahead of evaporation, membrane filtration for particulates, and recrystallization for final polish. Mother-liquor management is the quiet determinant of yield: recycle recovers residual lithium but accumulates impurities, so purge rate and wash discipline trade directly against product grade. Plants that treat the crystallizer as the only purity barrier discover that sodium control was won in the flowsheet around it.
From Wastewater Obligation to Urban Mine
The framing that has taken hold is accurate: high-salt lithium-bearing waste liquor is an urban ore. Operators now describe MVR systems turning industrial waste liquid into lithium feedstock, and integrated complexes combine dry pre-treatment with wet deep processing so lithium carbonate, lithium hydroxide, manganese sulfate, cobalt sulfate, and nickel sulfate all emerge from one material flow. For a recycler, the salt train is no longer a cost center; it is the last stage of the mine.
Feed Chemistry Changes the Train: Ternary Versus LFP
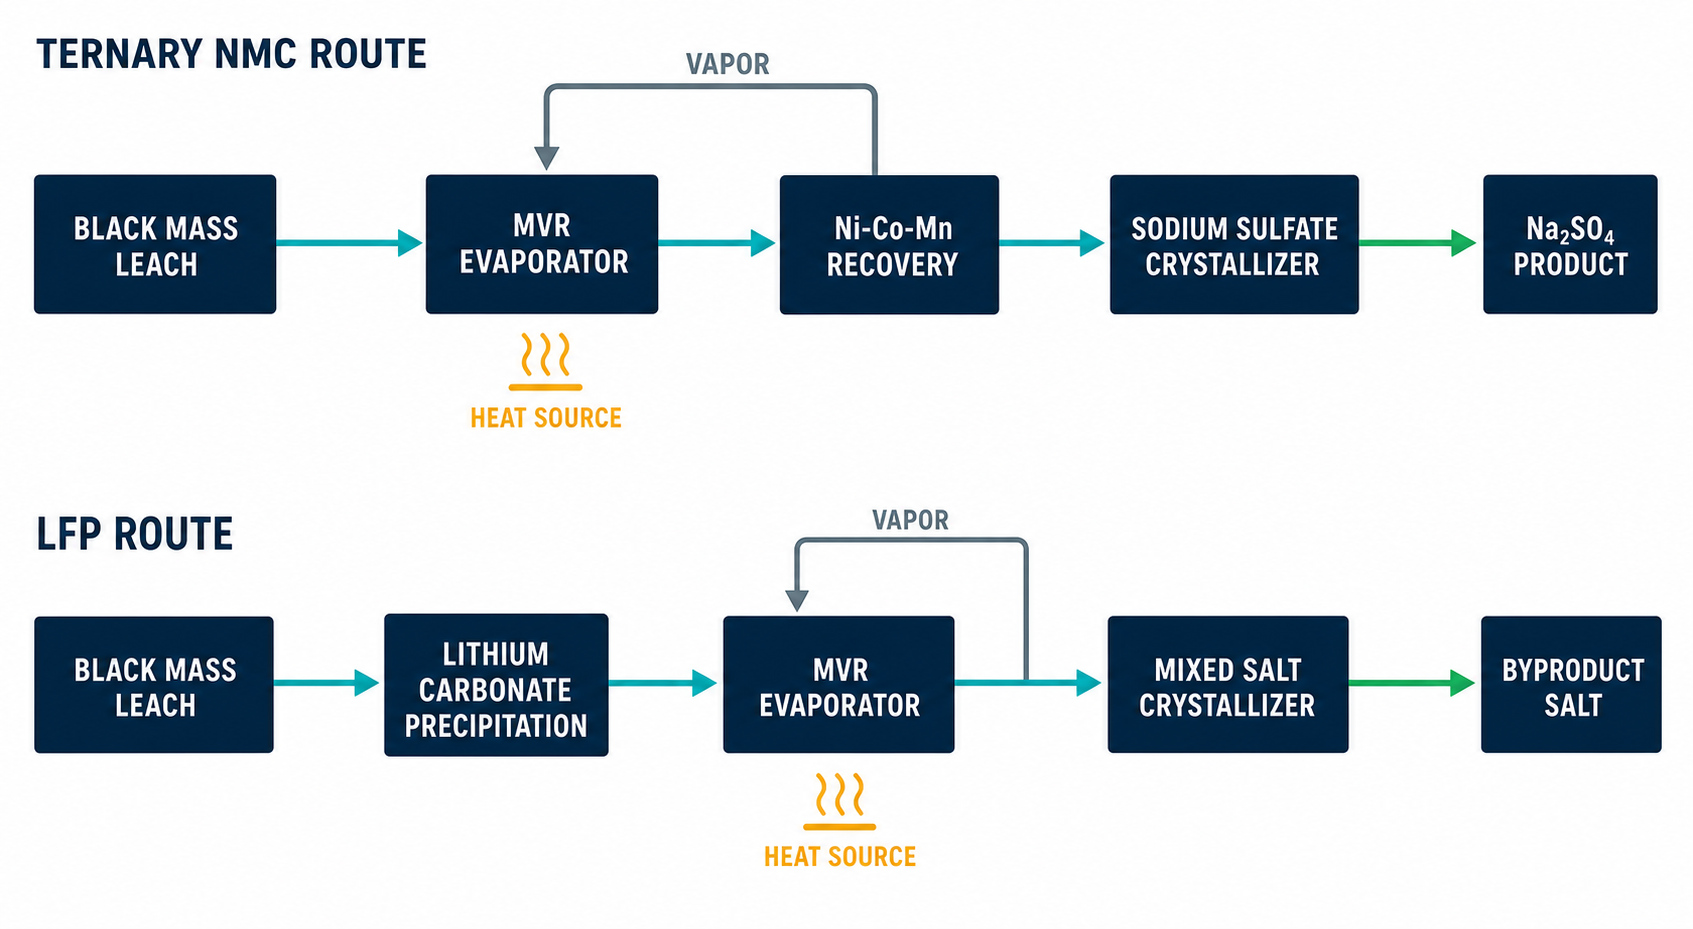
Ternary and LFP recycling impose different salt trains on the same evaporator core. Ternary black mass leachate carries three payable base metals plus lithium, so the flowsheet supports parallel nickel and cobalt lines of the kind the Korean project runs, with manganese through its own sulfate recovery and lithium precipitated from the end liquor. The salt load is sulfate-dominated, and sodium sulfate recovery is typically the largest byproduct stream by mass. LFP feed contains no nickel or cobalt to pay for the plant, so economics rest on lithium recovery from the precipitation mother liquor and iron phosphate reuse — which is why the 68-70 t/h MVR installations cluster in LFP complexes: water volume per tonne of payable metal is far higher, and only aggressive energy recycling keeps treatment affordable. Suppliers serving both feeds emphasize the same point from opposite directions: the evaporation core is standard, but the crystallizer sequencing, mother-liquor routing, and byproduct salt selection must be re-derived from the feed assay, not copied between chemistries.
When This Route May Not Fit
This train presumes a hydrometallurgical flowsheet with steady black-mass supply. Pyrometallurgical recyclers have no dilute leachate to concentrate. Small operators whose feed is measured in hundreds of tonnes per year cannot amortize MVR plus multi-salt separation. LFP plants at low lithium prices may find that recovery value no longer covers treatment, leaving simple brine disposal cheaper. And where recovered salts have no certified buyer — cathode producers audit recycled-material supply chains — the salt train reverts to a cost center regardless of technical success.
What Must Be Verified
Verification starts with the leachate assay across feed batches: metal ratios, acidity, and impurity envelope, since crystallizer sequencing is derived from it, never copied. Second, the target product grade — battery versus industrial — which sets purification depth and payback together. Third, phase-chemistry confirmation for the chosen salt sequence, ideally pilot-checked on the real mother liquor. Fourth, corrosion review against chloride and acid levels at temperature. Fifth, the lithium mass balance across mother-liquor recycle, trading recovery against impurity build-up. Sixth, the electricity-versus-steam price pair, and the downstream buyer’s certification requirements.
FAQ
Why does battery recycling need evaporation at all?
Acid leaching produces a large-volume, dilute metal liquor. Evaporation concentrates metal ions five to ten times, cutting reagent and energy demand in downstream precipitation, solvent extraction, or electrowinning, and returns condensate for reuse in leaching and rinsing.
What salts are recovered from lithium battery recycling wastewater?
Depending on the feed and flowsheet: nickel sulfate and cobalt sulfate as saleable battery-material crystals, sodium sulfate and sodium chloride as separated byproduct salts, potassium chloride where the stream carries it, and lithium returned as battery-grade carbonate or hydroxide.
What scale are these systems actually built at?
A published South Korean project runs 7.75 t/h on nickel solution plus 1.3 t/h on cobalt solution with forced-circulation evaporation and OSLO freeze crystallization, while Chinese LFP recycling complexes operate MVR trains at 68 and 70 t/h within 50,000 and 100,000 tonne-per-year plants.
How energy-intensive is MVR in this duty?
Supplier-reported figures run about 40-60 kWh per tonne of water evaporated at 50-70 degrees Celsius under vacuum, a 50-80% energy reduction versus steam-driven evaporation, with one project reporting payback shortening from three years to fourteen months.
Can recovered salts actually meet battery-grade purity?
Documented routes report lithium product purity of 99.5-99.9% with sodium chloride rejection above 99.5% and overall metal recovery above 95%, achieved through controlled crystallization, cold washing, precipitation, membrane polishing, and disciplined mother-liquor management.


