Centrifuge selection for crystal dewatering comes down to four coupled variables: the separation factor (G-force) the machine develops, the crystal size distribution the crystallizer delivers, the screen slot and back-flush regime, and the wash-water system — get all four right and a salt plant discharges a cake at 3–8% residual moisture that dries cheaply; get any one wrong and moisture creeps up, drying energy climbs, and product quality drifts. For coarse, robust crystals like salt and ammonium sulfate, pusher and peeler-type filtering centrifuges are the mainstream machines; for sludges, fines-rich brines and wastewater duties, the decanter (solid-bowl scroll) centrifuge is the workhorse. This guide walks the whole chain: machine types, the physics of separation factor, quantitative benchmarks for residual moisture, washing, troubleshooting, and how dewatering choices ripple into the dryer downstream.
Where Dewatering Sits and Why It Pays
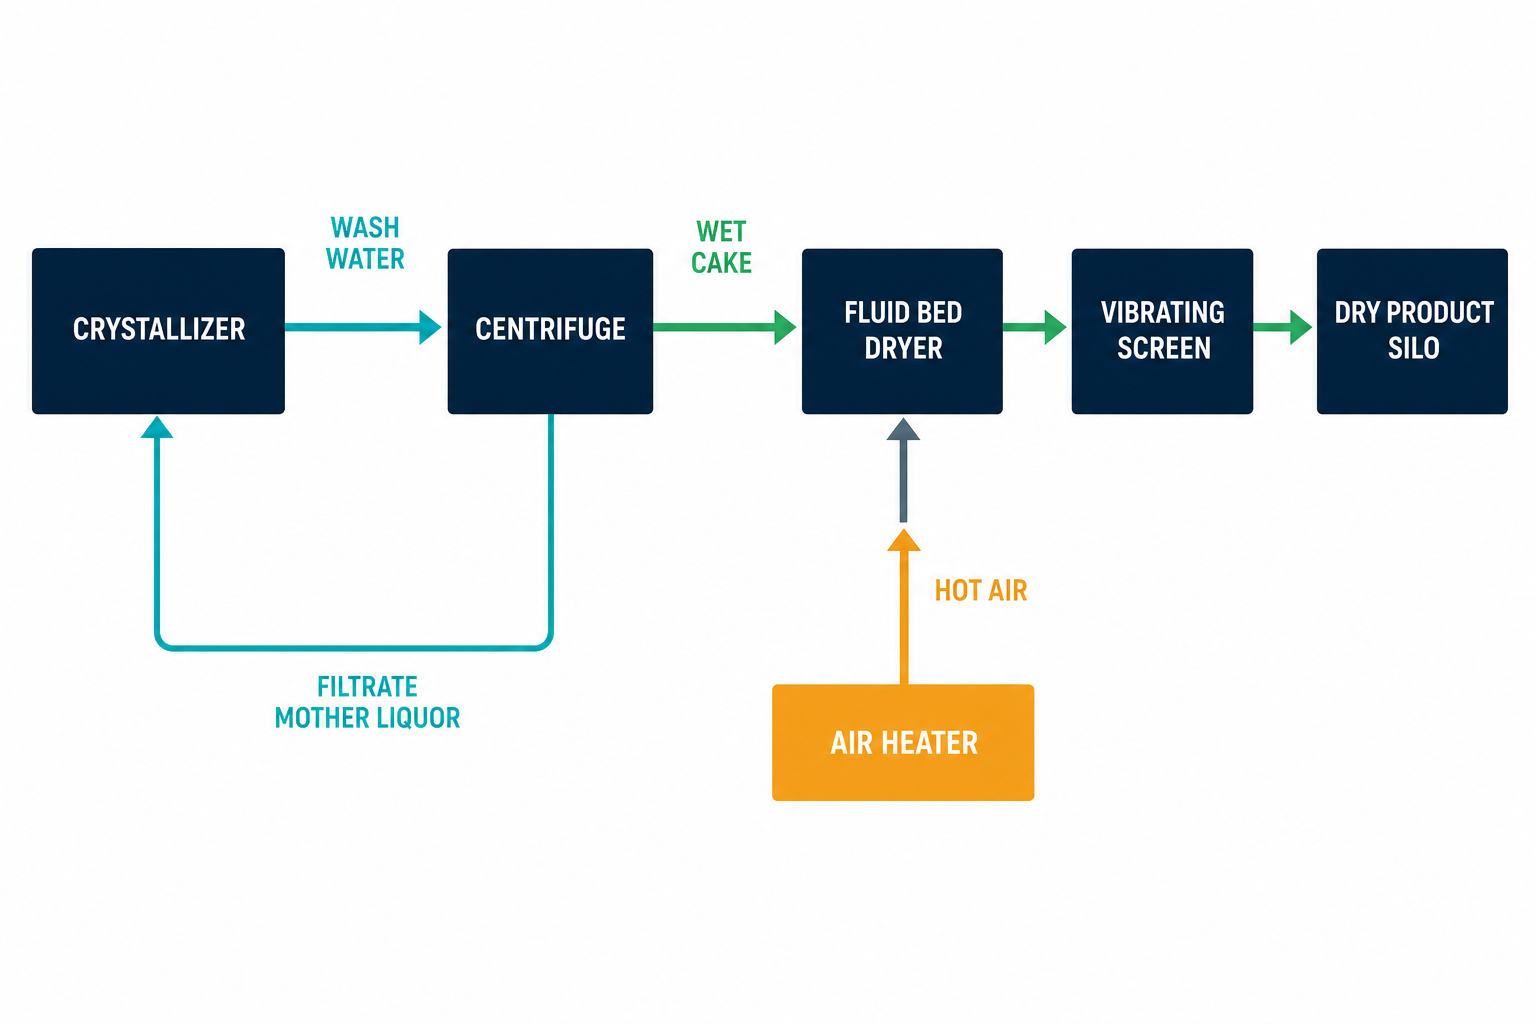
The crystallizer discharges a slurry; the centrifuge converts it to a wet cake; the dryer takes the cake to spec. Mechanical dewatering removes water at a fraction of the energy cost of thermal drying, so the centrifuge is the leverage point of the whole solids train: every percentage point of residual moisture removed mechanically is a percentage point the dryer does not have to evaporate. Residual moisture after centrifugation typically lands at 3–8% for well-formed salt crystals; filter cakes from closed filtration equipment hold 5–20% solvent. Design the sequence as a system — crystallizer CSD control first, then centrifuge selection (separation factor, screen), then wash and back-flush configuration, then matching the dryer’s capacity to the actual cake moisture — rather than buying each unit against isolated spec sheets.
The Decanter Centrifuge: Structure and Principle
A decanter (horizontal spiral centrifuge) consists of a rotating bowl and a screw conveyor rotating in the same direction at a slightly different speed. Feed slurry enters through a hollow shaft into the bowl; centrifugal force settles the solids against the bowl wall; the screw conveys the settled solids continuously toward the conical end for discharge, while clarified liquid overflows weir plates at the large end. There is no filter medium — separation is by sedimentation, which is why decanters handle fine, soft, or compressible solids that would blind a screen.
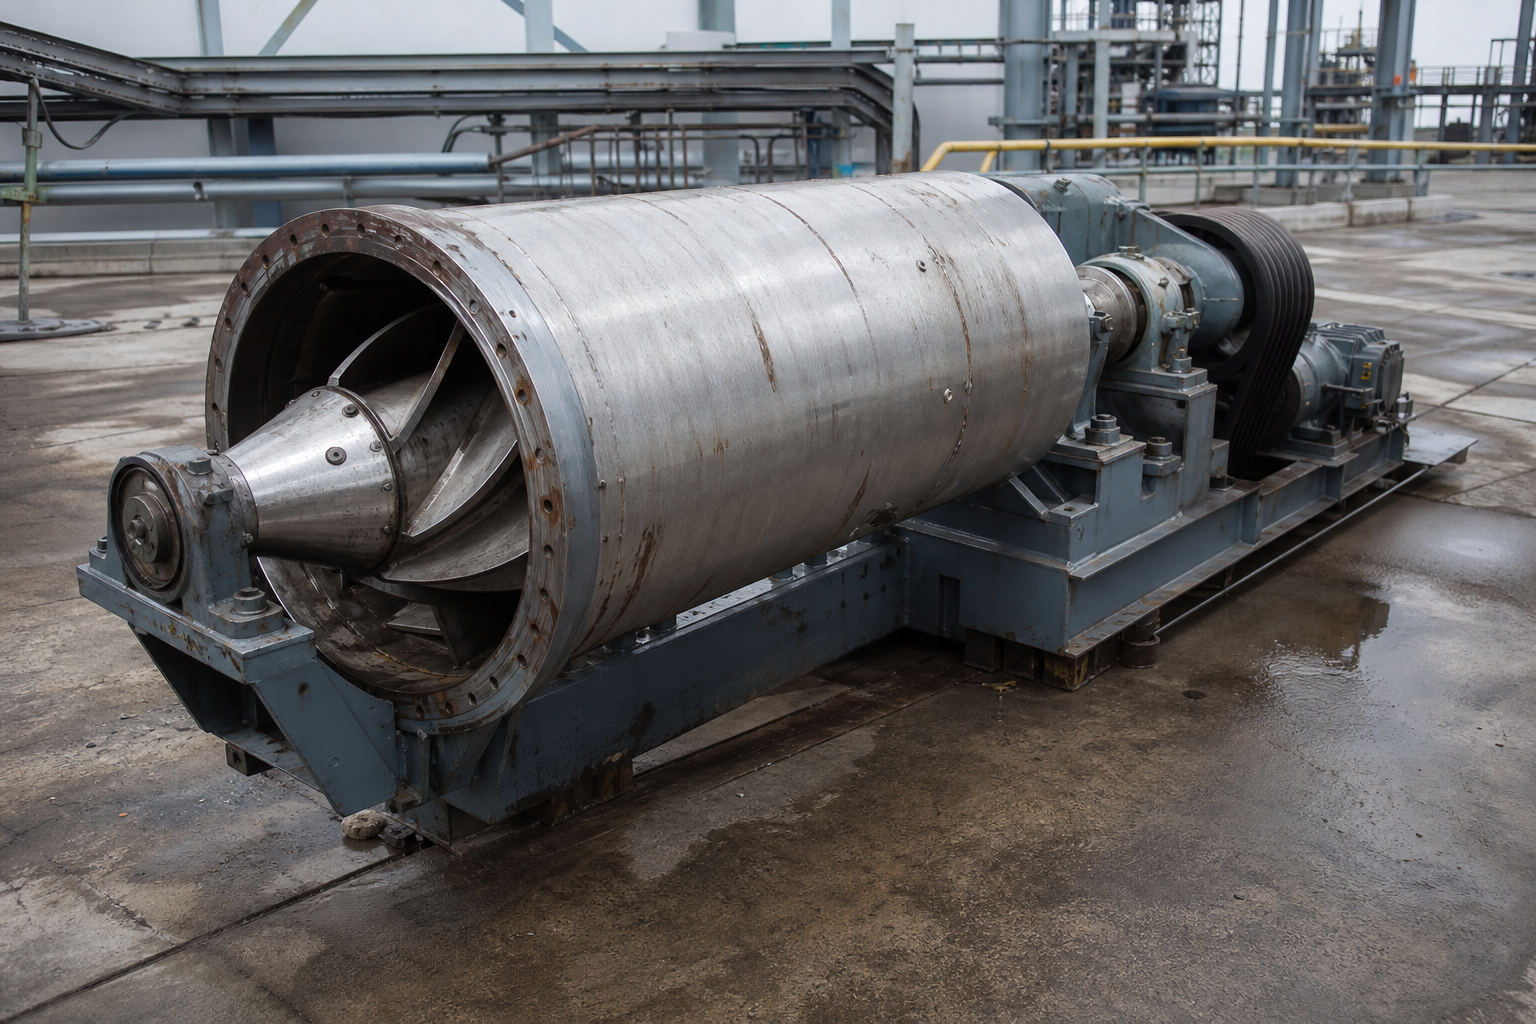
Key selection geometry includes the separation factor (G-force), bowl length-to-diameter ratio (L/D), beach angle, and wear/corrosion provisions such as ceramic inserts protecting the scroll discharge zone. Longer bowls give finer clarification; steeper beaches give drier cake at the cost of conveying torque.
The Two Parameters That Govern a Decanter
- Separation factor (G-force) — the centrifugal acceleration expressed as a multiple of gravity — determines what the machine can capture at all: finer particles demand higher G or flocculation assistance.
- Differential speed between bowl and screw sets solids residence time on the beach: higher differential moves solids out faster but leaves them wetter; lower differential dries the cake harder but raises torque and risks overload. Modern plants let the PLC trim differential speed against torque in real time.
Machine Families for Crystal Dewatering
| Machine | Mode | Best Fit | Watch-outs |
|---|---|---|---|
| Pusher centrifuge (single/two-stage) | Continuous, screen-based | Coarse, robust, free-draining crystals: salt, ammonium sulfate, potassium salts | Needs uniform, sufficiently coarse feed; fines leak through screens |
| Peeler / basket (three-column, scraper) | Batch, screen-based | Batch crystallization products needing wash and heel control | Batch throughput limits on very large duties |
| Solid-bowl decanter | Continuous, sedimentation | Sludges, fines-rich brines, corrosive or abrasive slurries | Cake always carries more surface moisture than screen machines; no washing of crystal purity |
| Filter press | Batch, pressure filtration | Fine slime, low-feed-solids duties where a dry cake matters more than crystal form | Discontinuous; not for crystal-product duties |
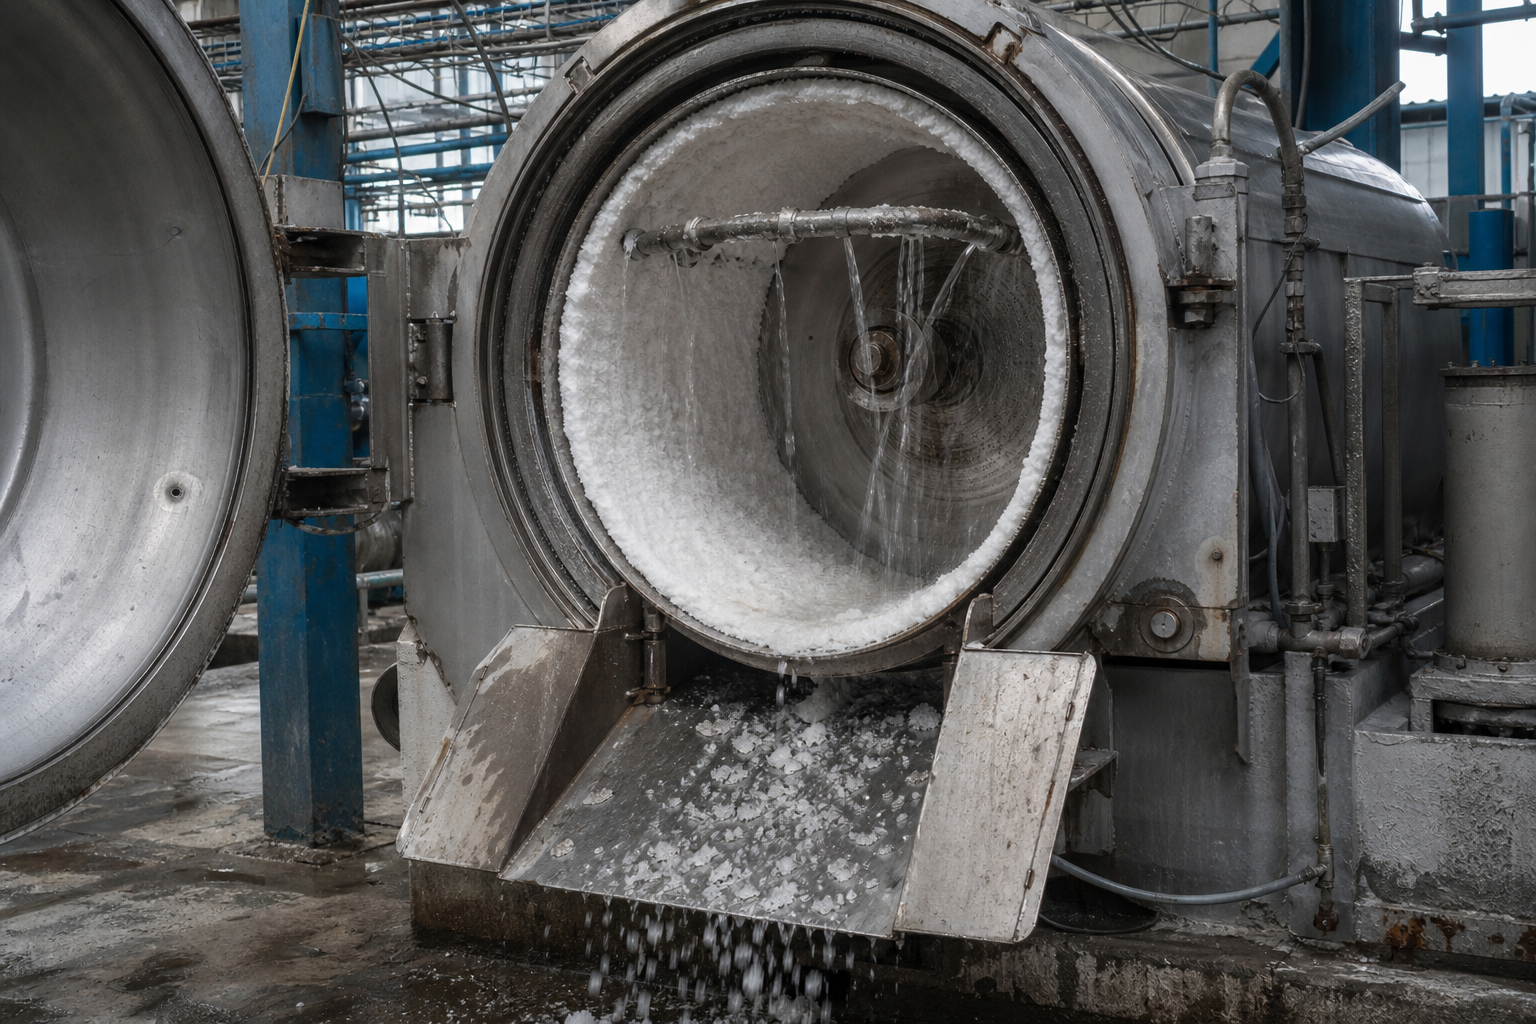
In salt service specifically, two-stage pusher centrifuges dominate continuous plants because salt crystals are coarse and strong enough to survive the pushing action while draining freely through 0.1–0.2 mm slotted screens. Upstream, the machine that made those crystals is usually an FC crystallizer or an OSLO/DTB unit — the choice among them directly shapes the feed the centrifuge sees.
Four Factors Behind Residual Moisture
1. Separation factor
Defined as bowl peripheral speed squared divided by gravitational acceleration, the separation factor sets the ceiling on dewatering. Industrial salt dewatering typically requires Fr ≥ 1,000, with high-specification duties running 2,000–3,000. Higher Fr lowers residual moisture but raises the risk of crystal breakage — on friable products there is a sweet spot, not a maximum.
2. Crystal size and distribution (CSD)
An average particle size ≥ 0.5 mm with a coefficient of variation ≤ 40% keeps filter-cake channels open and draining. When fines below 0.3 mm make up a significant fraction, cake permeability collapses and moisture climbs no matter how hard the machine pulls. This is why CSD problems are diagnosed at the centrifuge but solved at the crystallizer.
3. Screen selection and back-flushing
Screen slot widths of 0.1–0.2 mm are matched to the crystal size distribution. Blinding reduces the open area silently; periodic back-flush — typically every 15–30 minutes, for 30–60 seconds, at 0.3–0.6 MPa — restores throughput and is a scheduled necessity, not an emergency response.
4. Wash-water operation
Covered in the next section: wash quantity and temperature both move residual moisture and mother-liquor impurities simultaneously, in opposite directions from OPEX.
Quantitative Benchmarks at a Glance
| Variable | Working Range | Effect |
|---|---|---|
| Residual moisture, centrifuge discharge | 3–8% (crystal salts) | Each point saved is thermal load removed from the dryer |
| Separation factor, industrial salt | Fr ≥ 1,000 (2,000–3,000 high-spec) | Higher Fr = drier cake, more crystal breakage risk |
| Crystal size for good drainage | ≥ 0.5 mm mean, CV ≤ 40% | Fines < 0.3 mm collapse cake permeability |
| Screen slot | 0.1–0.2 mm, matched to CSD | Wider loses crystals; narrower blinds |
| Back-flush | 15–30 min interval, 30–60 s duration, 0.3–0.6 MPa | Maintains effective open area |
| Wash water | 5–15% of mass; 50–70°C | Removes Ca²⁺/Mg²⁺/SO₄²⁻ impurities; excess dilutes mother liquor and raises evaporation load |
Centrifugal Washing: Purity Versus Energy
Wash water displaces mother liquor from the crystal surface, removing calcium, magnesium and sulfate impurities. Two levers matter: quantity — typically 5–15% of the crystal mass — and temperature, with 50–70°C wash water lowering viscosity and improving displacement. The trade is explicit: every liter of wash that passes through ends up in the mother liquor, diluting it and adding to the evaporation load back upstream. Wash design is therefore an optimization between product purity spec and evaporator energy, not a maximization.
Troubleshooting High Residual Moisture
When moisture runs persistently high, work the chain in this order — each step is progressively more expensive to fix:
- Screen blinding — inspect and verify back-flush pressure and frequency first; it is the cheapest cause.
- Feed particle-size drift — sample the crystallizer discharge; a fines shift means the problem is made upstream, in the crystallizer’s supersaturation control.
- Insufficient separation factor — confirm bowl speed and, on decanters, differential speed against torque; only then consider re-rating the machine.
- Wash-water temperature too low — cold wash raises liquid viscosity and leaves the cake wetter while removing less impurity.
Coupling with the Dryer
The centrifuge and dryer should be quoted as a pair. A cake at 3% moisture versus 8% changes the dryer’s heat duty substantially, which changes its air system size, its energy draw and its footprint. Conversely, over-investing in G-force to chase the last point of moisture may break crystals into fines that the dryer then elutriates into the dust collection system. The economically correct design balances centrifuge CAPEX, crystal integrity and dryer energy as one problem — the dryer-side counterpart of this discussion is in industrial dryers for salt and crystal drying.
Decanters in Wastewater and Sludge Service
The same machine that fails to excite a salt marketer is indispensable at the plant’s back end. In wastewater treatment, decanters dewater municipal and industrial sludges from dilute 0.5–5% solids feeds into 20–35% solids cakes, and serve grit removal, grease separation and metal-bearing sludge recovery. Their strengths are continuous operation at high throughput, an enclosed casing that contains odor, high automation (PLC-controlled differential and torque), and a small footprint. Performance drivers are feed-solids consistency, particle fineness (fines need higher G or polymer flocculation), polymer dosing and mixing, and differential-speed setpoint — a large differential pushes solids out fast but wet.
In ZLD and high-salinity wastewater trains, the decanter typically handles the mixed-salt slurry that salt separation systems discharge, while screen machines handle the valuable single-salt streams; the dried product from either route exits through the drying and packing section.
FAQ
What residual moisture can a centrifuge achieve on salt?
Typically 3–8% residual moisture for well-formed salt crystals, depending on separation factor, crystal size distribution, screen condition and wash operation. Every percentage point saved here directly reduces the thermal load on the downstream dryer.
What separation factor is needed for industrial salt dewatering?
Fr ≥ 1,000 is the usual baseline, with 2,000–3,000 used for high-specification duties. Higher separation factor lowers moisture but increases crystal breakage, so friable products are optimized rather than maximized.
Pusher, peeler or decanter — which centrifuge for crystals?
Coarse, robust, continuous duties (salt, ammonium sulfate) go to pusher centrifuges; batch crystallization products needing wash control go to peeler baskets; sludges, fines and abrasive or corrosive waste slurries go to solid-bowl decanters. Very fine slime duties use filter presses instead.
Why does wash water temperature matter?
Hot wash (typically 50–70°C) lowers viscosity, improving displacement of mother liquor and impurity removal, and leaves a drier cake. The counterweight is energy: excess wash dilutes the mother liquor and increases the evaporator’s load upstream.
My cake moisture has crept up. What do I check first?
In order: screen blinding and back-flush operation, then feed particle-size drift from the crystallizer, then separation factor and differential speed, then wash-water temperature. The first two causes are the most common and the cheapest to fix.