Black liquor evaporation is the load-bearing step of a kraft mill’s alkali recovery cycle: it takes weak black liquor from the washing filters — an illustrative feed envelope of mid-teens to around twenty percent dissolved solids — and concentrates it to the high-solids liquor, commonly in the range of roughly two-thirds solids and above, that the recovery boiler needs to fire stably and self-sustainably. Everything downstream — boiler steam generation, cooking-chemical recovery, the mill energy balance — depends on it. A modern evaporation plant does this with multi-effect falling-film trains increasingly supplemented by MVR recompression, designed around the four enemies that define black liquor service — viscosity, fouling, boiling point elevation and boiler-feed stability.
What Black Liquor Is and Why Mills Concentrate It
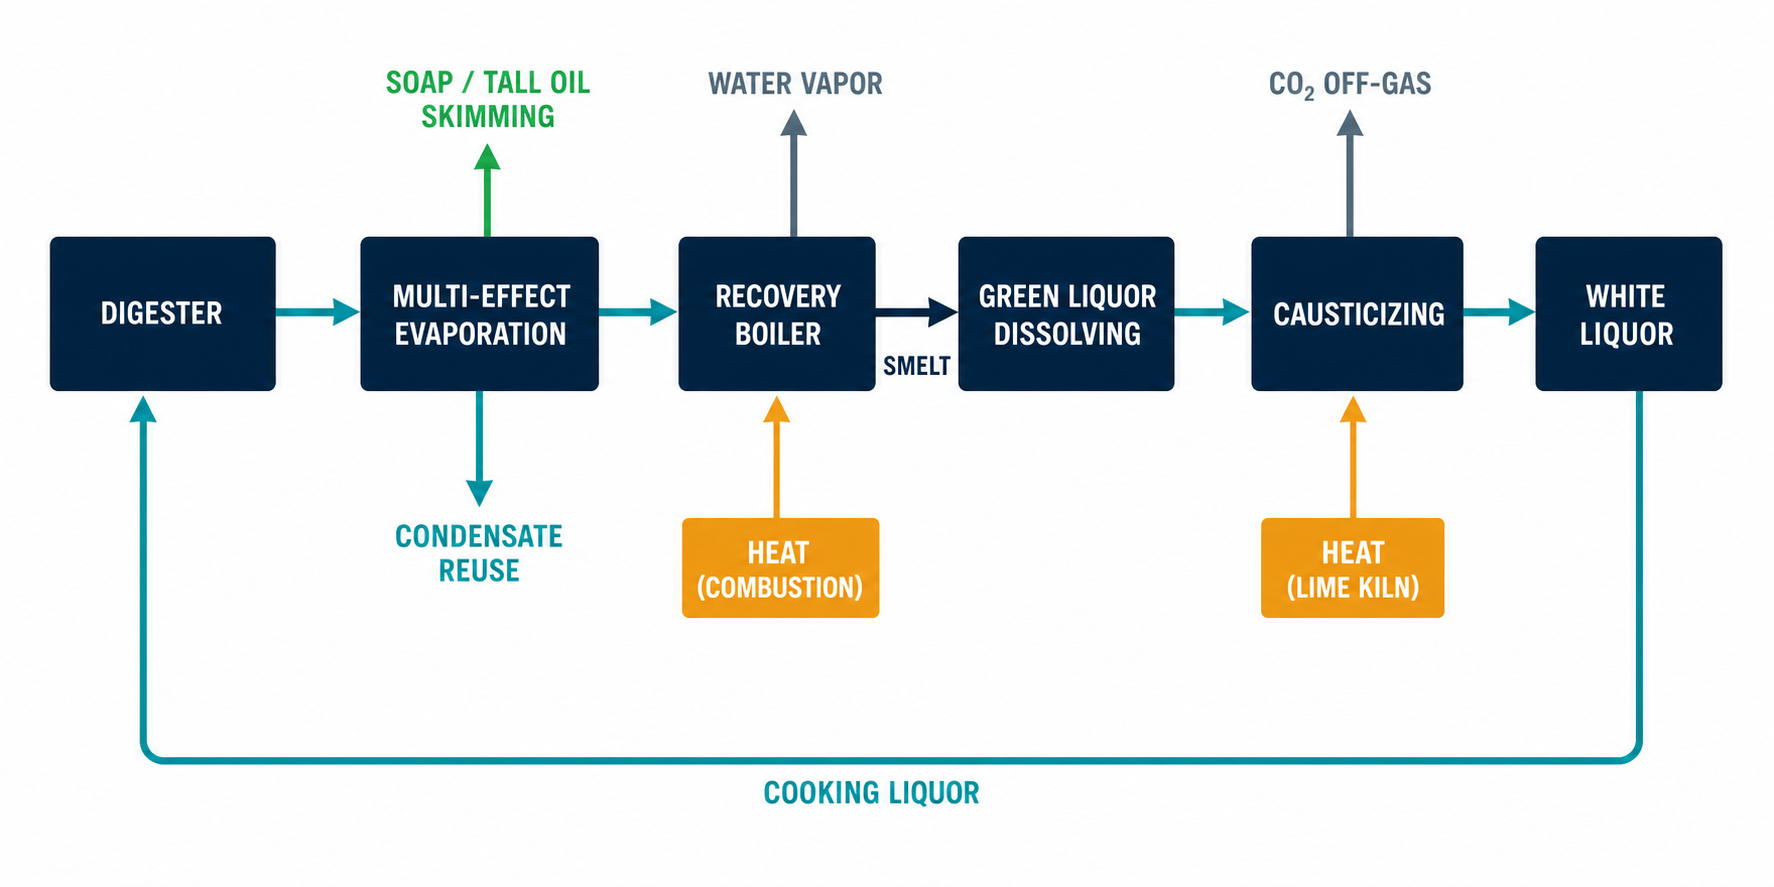
Black liquor is the spent cooking liquor of the kraft process: water carrying the lignin and hemicellulose fragments dissolved out of the wood, plus the inorganic cooking chemicals — predominantly sodium salts — and a share of extractives. As it leaves the digester and brown-stock washing, it is a hot, dilute, foamy liquid far too weak to burn. The recovery boiler is simultaneously a power boiler and a chemical reactor: it burns the organic fraction for energy and leaves the inorganic fraction as smelt, which is re-dissolved, causticized and returned to the digester as fresh white liquor. That double duty only works with concentrated feed — fire dilute liquor and the boiler consumes more energy evaporating water than the fuel value delivers. Hence the evaporation plant: it removes more water than any other single unit operation in the mill, and it does so at the lowest achievable energy cost, because every joule spent here propagates through the mill’s steam balance.
The Alkali Recovery Cycle in Context
Evaporation sits in the middle of a loop, and its performance is defined by the neighbors on both sides.
| Loop stage | What happens | What it needs from evaporation |
|---|---|---|
| Washing | Brown stock washing recovers weak black liquor from the pulp | Accept variable feed solids and temperature without upset |
| Evaporation | Weak liquor concentrated to firing solids in multi-effect or MVR trains | — |
| Recovery boiler | Organics burned for energy; inorganics leave as smelt | Stable, predictable outlet solids; no fluctuations |
| Causticizing | Smelt dissolved to green liquor; causticized to white liquor | Steady soda balance in the fired liquor |
The boiler is the least forgiving customer in the mill. If outlet solids fluctuate, recovery-boiler operation becomes harder to control — the reason mill engineers treat evaporator stability as a boiler-safety and availability issue, not a process nicety.
The Four Engineering Challenges of Black Liquor Evaporation
1. High viscosity at high solids
As solids rise, black liquor viscosity climbs steeply — the liquor turns into a heavy, shear-sensitive syrup. High viscosity limits circulation through the heating bodies and reduces effective heat transfer exactly where the concentration duty is hardest. The design answers are large-cross-section falling-film bodies, generous circulation where forced circulation is used, and careful attention to liquor temperature, because black liquor viscosity is strongly temperature-dependent: hotter operation keeps the liquor pumpable at solids levels that would gel at lower temperature.
2. Fouling and scaling
Deposits build on the heating surfaces — calcium carbonate scales from the liquor’s hardness content, and at high solids, fouling becomes more aggressive as viscous, organics-laden liquor lingers near the wall. Fouling shortens run length between cleanings and silently erodes capacity. Countermeasures are well established: falling-film surfaces that keep liquor residence times short and wall temperatures low, robust clean-in-place systems designed for the real cleaning frequency, and intermediate final-effect arrangements that pull the fouling duty into bodies designed to tolerate it.
3. Boiling point elevation
Black liquor’s dissolved solids raise its boiling point well above that of water, and the elevation grows as concentration proceeds. Higher BPE reduces the temperature driving force available across each heating surface and raises steam demand — a thermodynamic handicap that no control strategy removes, only that sound body count and heat-transfer area can absorb. It is one of the main reasons black liquor plants historically run many effects in series and why the surface area margin between design point and end-of-run fouled condition is guarded so carefully.
4. Recovery boiler feed stability
The evaporation plant must deliver firing solids within a tight, predictable band, hour after hour. Solids measurement at the discharge, density inference, and forward-acting control on steam and feed — not just level control — are what keep the boiler’s char bed and steam production steady. Mills that cheap out here pay the price in boiler availability, which is the most expensive downtime in the plant.
Evaporator Configurations for Black Liquor
Two mechanical families dominate, with hybrid and retrofits common.
| Configuration | Role in black liquor service | Strengths | Trade-offs |
|---|---|---|---|
| Multi-effect falling-film train (MEE) | The workhorse: bulk concentration from weak liquor to intermediate/high solids across successive effects at descending pressures | Low specific steam consumption per effect added; proven at every scale; mature surface technology | Capital and footprint scale with effect count; live steam required |
| Forced-circulation finisher / concentrator | Final lift to firing solids where viscosity and fouling peak | Robust at the worst point in the concentration range; suppressed boiling protects surfaces | Higher specific energy than film bodies; pump power continuous |
| MVR recompression | New plants and retrofits where electricity is attractive; also used to upgrade existing MEE by adding MVR booster capacity | Cuts or eliminates live-steam demand; supplier-reported energy reductions above 60% in comparable duties — indicative range, not a project guarantee | Compressor capital and maintenance; economics depend on electricity-versus-steam price |
| Thermal compressor (thermocompressor) effects | Steam-economy upgrades on existing plants | Simple, no moving parts, long service life | Motive steam consumption; fixed compression ratio |
The typical modern flow sheet stacks these: falling-film effects for the bulk water removal, a forced-circulation finisher for the last stretch of solids, and increasingly an MVR stage or booster on the multi-effect train to relieve the mill’s steam balance — the same retrofit logic we apply in energy retrofit and decarbonization projects.
| Process module | Equipment candidates | Selection basis | Indicative envelope |
|---|---|---|---|
| Weak-liquor handling, soap skimming | Feed tank; skimming stages | Extractives recovery, pitch control | Mid-teens to ~25% solids feed |
| Bulk concentration | Falling-film multi-effect bodies | Steam economy, moderate viscosity | To intermediate-high solids |
| Final concentration | Forced-circulation finisher | Peak viscosity, fouling | To ~two-thirds solids |
| Condensate handling | Split headers; methanol stripper | Methanol recovery, water balance | Clean/foul split |
Configuration, materials and envelopes depend on actual feed, fouling behavior, steam balance and target capacity.
By-Products Recovered Along the Way
A black liquor evaporation plant is also a separation plant. Crude sulfate soap — the resin and fatty acid extractives that float out of kraft liquor at intermediate solids — is skimmed in soap separation stages and becomes tall oil, a saleable raw material for the tall-oil distillation industry; well-run soap recovery both earns revenue and protects downstream surfaces from pitch fouling. Methanol and turpentine bearing condensates from the effects are stripped and recovered rather than lost to the sewer. In modern biorefining concepts, the evaporation plant is additionally the gateway for lignin extraction, where precipitated lignin is filtered from the liquor and sold as a renewable material. The evaporation designer who treats these sidestreams as afterthoughts leaves money and operability on the table.
Condensate Strategy and the Mill Water Balance
Effect condensates are hot water in tons per minute, and how the plant segments them — clean secondary condensate reused as boiler-feed makeup, showers and lime-loop water; fouler primary condensate segregated and stripped — is where the operating economics live. Methanol-bearing foul condensate is stripped in dedicated strippers, recovering methanol as fuel for the mill and cleaning the condensate for reuse. A well-segregated condensate system is what allows the mill to close its water balance without contaminating it.
Design and Operating Notes from Mill Practice
- Size the surface for end-of-run, not start-of-run. Heat-transfer coefficients decay between cleanings; a body sized on clean coefficients fails its duty cycle within months.
- Treat solids control as a boiler contract. Discharge-solids instrumentation with forward-acting steam and feed control keeps the firing solids inside the band the recovery boiler was certified for.
- Design the CIP for the actual fouling rate. Cleaning frequency, not cleaning chemistry, decides annual capacity; bodies and headers must be piped for the frequency the liquor actually demands.
- Watch viscosity-temperature interaction at the finisher. Higher firing solids are reachable when liquor temperature is held up; letting it sag gels the finisher.
- Plan soap removal deliberately. Soap carried past its separation window fouls everything downstream and surrenders tall-oil value.
How EvapCryst Delivers Black Liquor Evaporation Projects
EvapCryst engineers evaporation and concentration systems for high-viscosity, fouling-prone organic-inorganic liquors — black liquor being one of the defining cases of the type. We configure falling-film and forced-circulation bodies around your target solids, mill capacity and energy balance, with circulation design and heat-transfer surfaces selected to keep performance stable as viscosity rises — the difference between meeting the solids specification in March and still meeting it after a year of campaign fouling. Our work spans the mill-adjacent duties described on the pulp and paper industry page, and the same viscous-organic handling competence appears in duties like emulsion and oily wastewater evaporation. Required inputs: the weak-liquor analysis, the firing-solids target and the mill steam balance — in exchange, an initial process direction covering effect count, surface split and an indicative energy budget.
When This Route May Not Fit
This route assumes a kraft mill with a recovery boiler in the loop. It may not fit when the plant is a small non-wood mill — straw and reed liquors carry high silica, which changes scaling behavior fundamentally and pushes the design toward non-standard solutions. It may not fit when liquor throughput is too small to carry the fixed surface of a multi-effect train, or when the mill has no recovery boiler and the goal is wastewater volume reduction rather than chemical recovery — thermal concentration without the recovery loop rarely pays for itself. And an MVR booster loses its case where electricity is expensive relative to steam, or where the mill already vents surplus low-pressure steam. Plants with no spare footprint or crane access may also rule out finisher retrofits.
What Must Be Verified
Before a route is fixed, the validation focus falls on five items. First, a full weak-liquor analysis: solids, alkali profile, and — critically — the viscosity-temperature curve at firing solids and the boiling-point-elevation curve, because these two curves size the bodies. Second, scale-former content: calcium and, for non-wood mills, silica, which set the fouling-rate assumption behind the end-of-run heat-transfer coefficients. Third, the firing-solids target as certified by the recovery-boiler vendor, not as wished for. Fourth, the mill’s steam and power balance, which decides between multi-effect alone and an MVR booster. Fifth, condensate reuse specifications — how much methanol the boiler-feed makeup can tolerate — and the soap-skimming window at intermediate solids. Lab analysis and reference-plant operating data, not supplier catalogs, are the evidence base.
FAQ
Why does black liquor need to reach such high solids before firing?
The recovery boiler burns the organic fraction to make steam and recovers the inorganic fraction as smelt. Dilute liquor would spend much of its fuel value evaporating its own water, so mills concentrate from roughly the mid-teens in solids to around two-thirds and above, where the liquor fires self-sustainably and the boiler’s steam and smelt output meet design.
What limits black liquor evaporation capacity in practice?
Fouling and viscosity, jointly. Deposits on heating surfaces raise the effective resistance to heat transfer and shorten run time, while rising viscosity at high solids limits circulation. Plants manage both through falling-film surfaces, forced-circulation finishers, liquor temperature control and clean-in-place systems sized to the real fouling rate.
Is MVR suitable for black liquor, or is multi-effect the only option?
Multi-effect falling-film trains remain the backbone of black liquor concentration, but MVR has a growing role — in new plants where electricity is attractive, and especially as retrofit booster capacity that relieves live-steam demand on existing effects. External supplier references report MVR energy reductions above 60% in comparable duties — a supplier-published indicative range, not a project guarantee.
What is boiling point elevation and why does it matter here?
Dissolved solids raise the boiling point of the liquor above that of pure water, and the gap widens as concentration proceeds. Every degree of BPE is driving force lost across the heat surfaces and steam demand added, so it shapes effect count, heat-transfer area and steam economy.
Can a black liquor evaporation plant earn revenue, not just save cost?
Yes. Sulfate soap skimmed at intermediate solids becomes tall oil for sale; stripped methanol from foul condensate returns as fuel; and in biorefining configurations, lignin withdrawn from the liquor becomes a saleable renewable material. These sidestreams are designed in, not incidental — soap separation in particular protects downstream surfaces while it earns.