Polyoxymethylene (POM) Production Integration
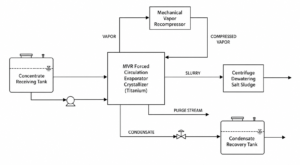
Integrated POM plant solutions covering formaldehyde concentration, trioxane purification, inert powder drying and formaldehyde wastewater closure – engineered as one heat and material balance.
Selection logic, retrofit economics and mother-liquor yield — articles from three lines: technology deep-dives on evaporator and crystallizer selection, application solutions for specific wastewaters and process duties, and anonymized project case studies. New articles are published continuously.
Technology ArticlesApplication SolutionsProject Case Studies

Integrated POM plant solutions covering formaldehyde concentration, trioxane purification, inert powder drying and formaldehyde wastewater closure – engineered as one heat and material balance.

Representative configuration of a 40 t/h six-effect falling-film evaporation train with continuous sterilization duty, supplying concentrated glucose feed to a large new threonine fermentation

Two-stage concentration (multi-effect/MVR falling film plus low-temperature finish) and controlled cooling crystallization recover more xylose from corn-cob hydrolysis liquor at lower energy per ton.

Representative configuration of a 42.24 t/h glucose syrup concentration train in East China (Shandong): MVR with five-effect falling-film evaporation, with comparable deployments at 70

Four-effect TVR falling film evaporation for instant coffee: 4-5 Brix extract to 45 Brix concentrate at ~3.9 kg water per kg steam. Enlarged separators,

Why 90-95% factory prefabrication, 50-60% shorter field installation, and 35-50% smaller footprints make skid-mounted MVR evaporators and crystallizers the default for modern plant upgrades

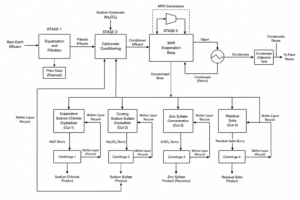
Representative configuration of an MVR evaporation system separating four salts (NaCl, Na2SO4, Na2CO3, ZnSO4) from rare earth separation effluent at 150 t/d in North

MVR evaporation and crystallization in lithium battery recycling: 5-10x leachate concentration, NiSO4/CoSO4 crystal recovery, salt separation, and project data from 1.3 to 70 t/h

The ZLD end stage decides project economics: mixed salt is fee-charged hazardous waste while separated NaCl (GB/T 5462) and Na2SO4 sell. MVR vs seed-slurry

Representative configuration of a 60 m³/d MVR forced-circulation evaporation crystallization train in Baotou, Inner Mongolia, treating high-salt RO membrane concentrate from rare earth separation
Send your feed characterization (TDS, COD, main salts, viscosity), throughput and product targets — we respond with a preliminary process route within two business days.